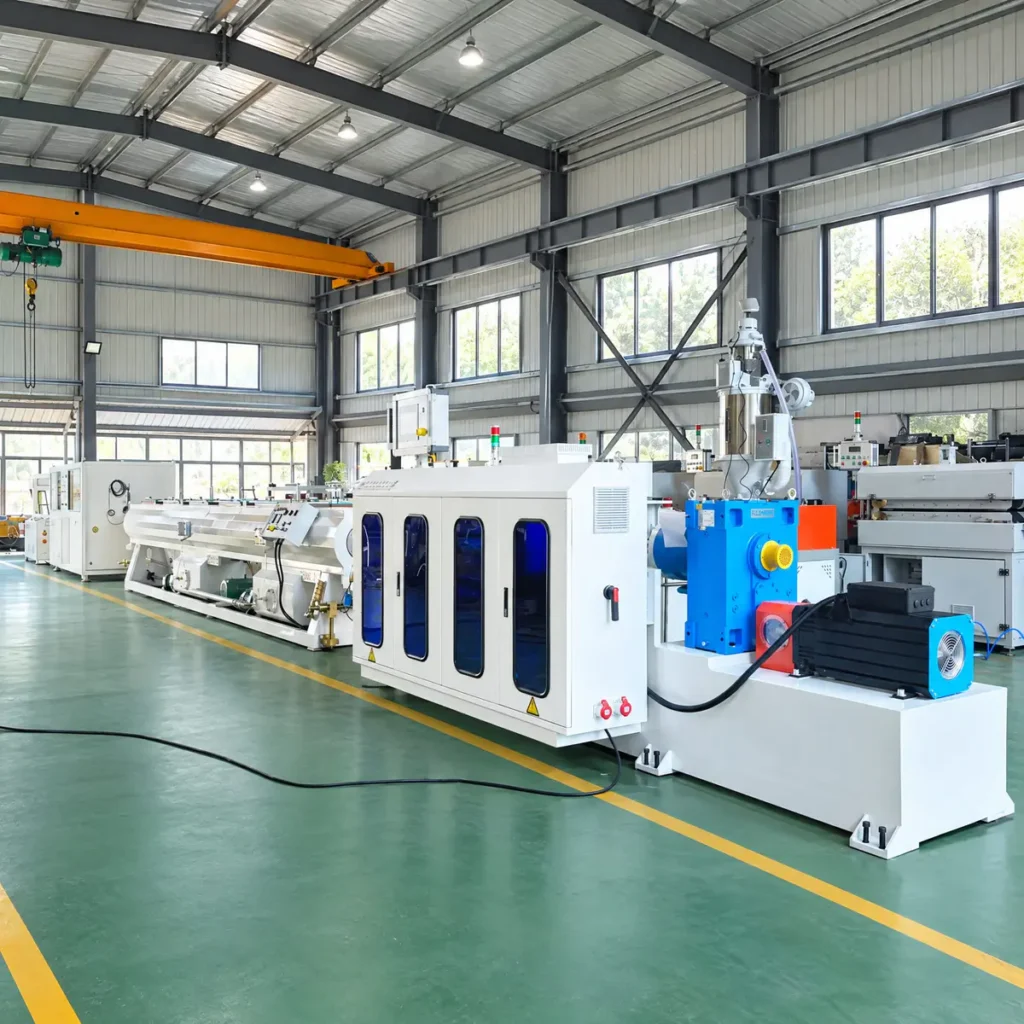
What is a PE Core Pipe Extrusion Line Used For?
Learn how a PE core pipe extrusion line produces strong roll core tubes for film, foil, packaging, and industrial winding applications.
1. What is a PE core pipe extrusion line used for?
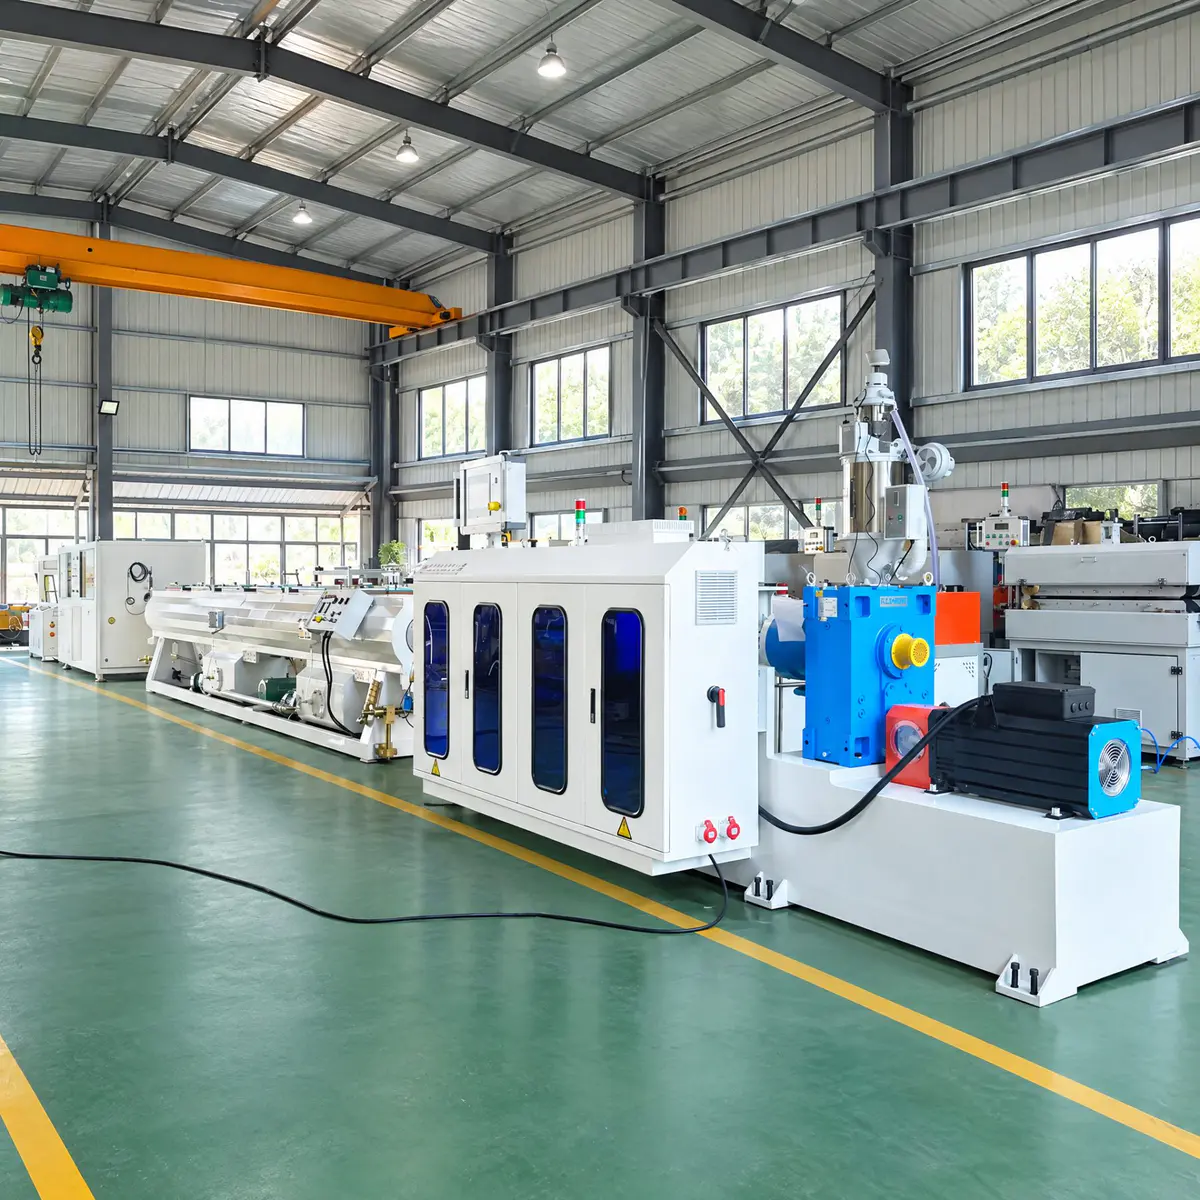
A PE core pipe extrusion line is used to produce PE roll core tubes for winding film, foil, packaging materials, electronic materials, and other industrial rolls.
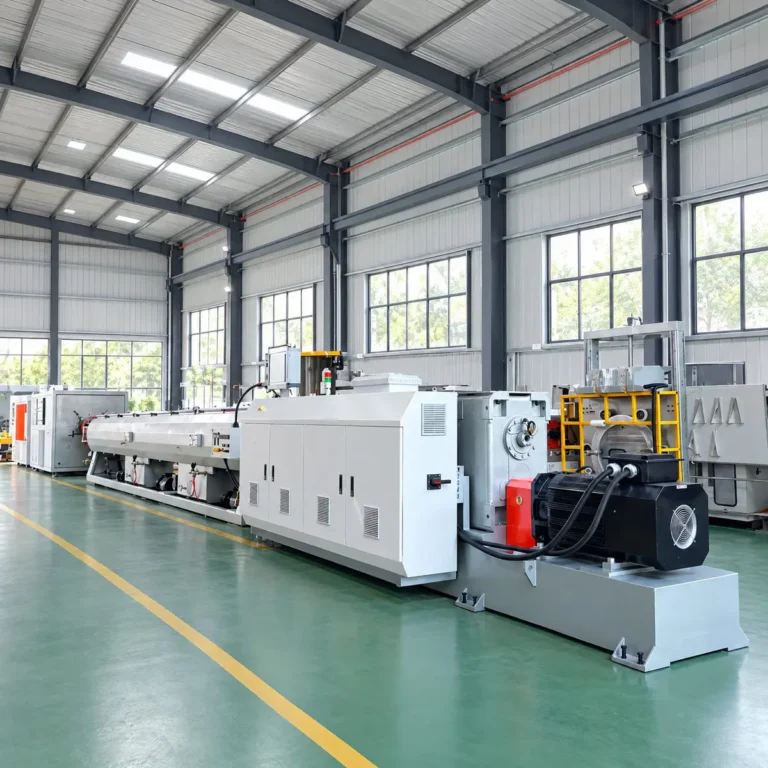
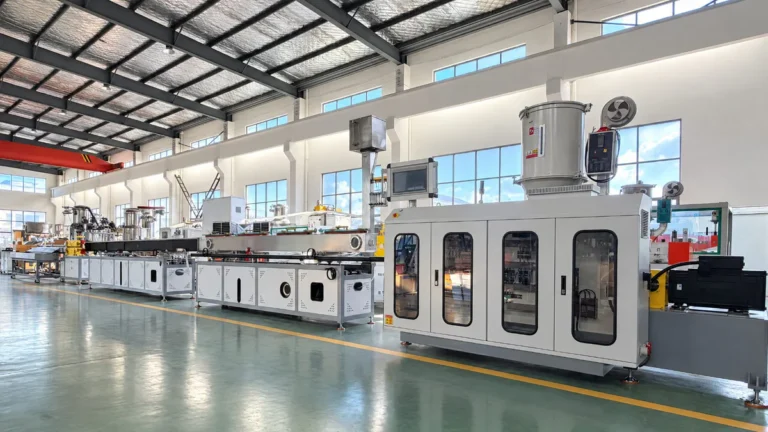
A PE core pipe extrusion line is a complete production system that melts PE or HDPE material, forms it into a hollow pipe, calibrates the pipe size, cools it, pulls it forward, measures the length, and cuts it automatically.
Unlike ordinary water pipe production, PE core pipe production focuses more on:
- Roundness
- Wall thickness stability
- Pipe rigidity
- Accurate cutting length
- Smooth pipe ends
- Stable winding performance
These PE core pipes are commonly used as roll support cores in industries such as:
- Plastic film rolls
- Aluminum foil rolls
- Packaging material rolls
- Electronic material winding
- Industrial sheet and tape rolls
In the QTech-Machinery customer case, the line was designed for producing PE roll core tubes with an inner diameter of around 77 mm and multiple wall thickness options, including 6 mm, 7 mm, 8 mm, 9 mm, and 10 mm.
Recommended internal links:
2. What products can be made by a PE core pipe extrusion line?
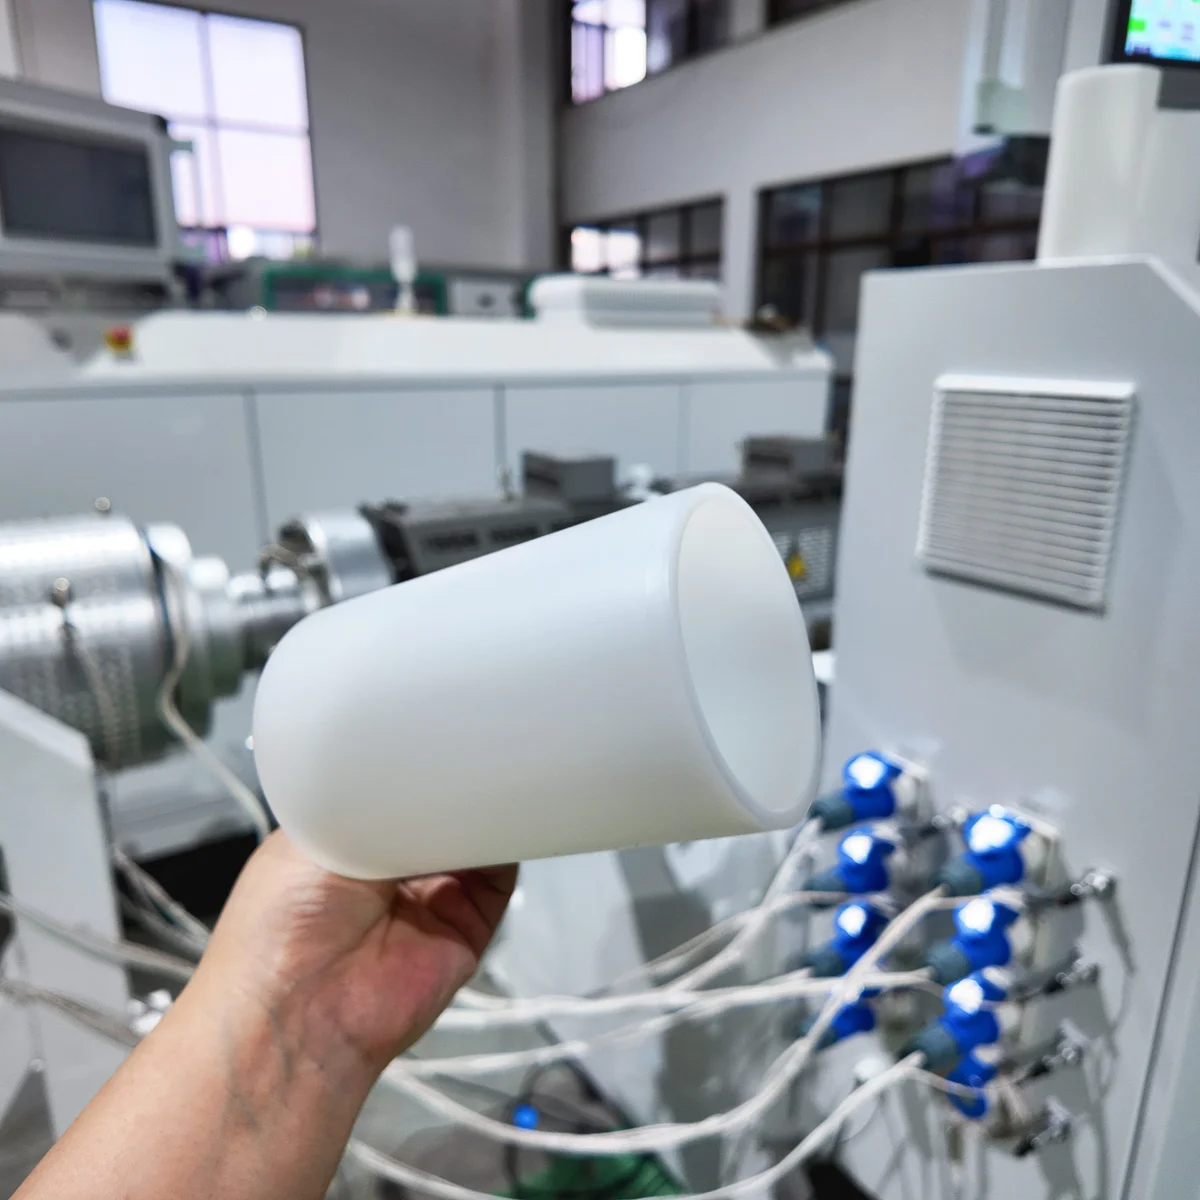
This line mainly produces PE core pipes, PE roll core tubes, and PE winding core pipes for industrial roll applications.
The final product is a rigid PE pipe used as the center core for winding materials. Compared with paper cores, PE core pipes can offer better moisture resistance, stronger structure, and longer service life in some industrial applications.
Typical products include:
| Product Name | Common Application | Key Requirement |
|---|---|---|
| PE Core Pipe | General industrial roll support | Strength and roundness |
| PE Roll Core Tube | Film, foil, packaging roll winding | Smooth surface and stable size |
| PE Winding Core Pipe | Electronic material and precision roll winding | Accurate length and clean pipe end |
| HDPE Core Tube | Heavier roll support | Higher rigidity and wall thickness |
For customers producing roll core tubes, the pipe must support winding pressure without deformation. This is why the extrusion line must combine stable extrusion, accurate mould design, vacuum calibration, controlled haul-off, and chipless cutting.
3. What machines are included in a PE core pipe extrusion line?
A complete PE core pipe extrusion line usually includes an extruder, pipe mould, vacuum calibration tank, haul-off machine, encoder measuring system, and chipless cutting machine.
Based on the QTech-Machinery configuration, the production line includes the following main machines:
| Machine | Function | QTech-Machinery Configuration |
|---|---|---|
| SJ75/33 Single Screw Extruder | Melts and plasticizes PE material | 75 mm screw, 33:1 L/D, 45 kW motor |
| PE Core Pipe Mould | Forms the pipe shape | Customized for around 77 mm inner diameter |
| 160 Vacuum Calibration Tank | Sizes and cools the pipe | 9 m tank, vacuum range 0.02–0.08 MPa |
| Three-Claw Haul-Off Machine | Pulls the pipe continuously | Servo-driven traction, 0.2–3 m/min |
| Encoder Measuring System | Measures pipe length | Supports automatic fixed-length cutting |
| 160 Chipless Cutting Machine | Cuts pipe without chips | Suitable for 50–160 mm pipe diameter |
This configuration is suitable for producing thick-wall PE core pipes that require stable traction and accurate cutting.
4. How does the PE core pipe extrusion process work?
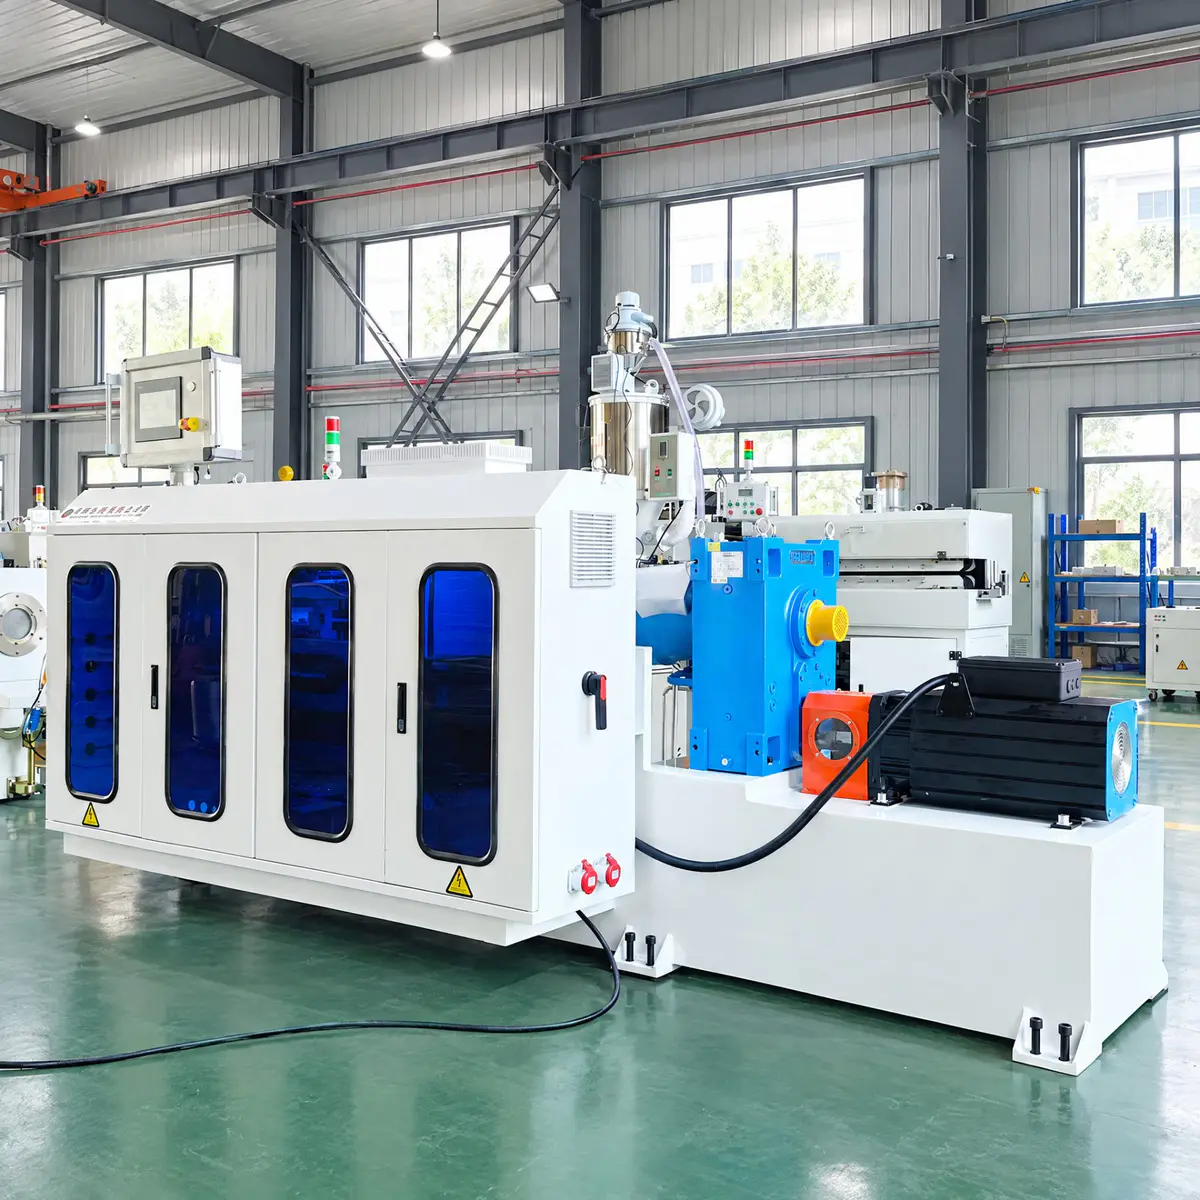
The process includes PE plasticizing, mould forming, vacuum sizing, cooling, hauling, encoder length measuring, and chipless cutting.
The production process can be divided into several practical stages:
Step 1: PE material feeding and plasticizing
PE or HDPE material enters the SJ75/33 single screw extruder. The screw and barrel heat, compress, and melt the material into a uniform plastic melt.
QTech-Machinery uses:
- 75 mm screw diameter
- 33:1 L/D ratio
- 38CrMoAlA nitrided screw and barrel
- 45 kW main motor
- Inverter speed control
- Segmented cast-aluminum heaters
These features help improve melt stability and continuous extrusion performance.
Step 2: Pipe mould forming
The melted PE material flows into the customized mould. The mould shapes the material into the required PE core pipe size.
For this customer case, the mould was designed for:
- Inner diameter around 77 mm
- Wall thickness options from 6 mm to 10 mm
- PE roll core tube production
Step 3: Vacuum calibration and cooling
After leaving the mould, the pipe enters the 160 vacuum calibration tank. Vacuum sizing helps maintain pipe shape and roundness, while spray cooling reduces pipe temperature and stabilizes dimensions.
Industry discussions about pipe extrusion often emphasize that vacuum repeatability, cooling uniformity, and haul-off stability are important for controlling OD, wall thickness, and ovality. [0]
Step 4: Continuous hauling
The three-claw haul-off machine pulls the pipe forward at a controlled speed. Stable haul-off is important because traction speed changes can affect wall thickness and pipe dimensions. [1]
Step 5: Encoder measuring and chipless cutting
The encoder measures the pipe length. When the target length is reached, the chipless cutter performs automatic fixed-length cutting.
Chipless cutting is useful for PE core pipe production because it helps reduce:
- Cutting dust
- Material waste
- Pipe-end burrs
- Cleaning work after cutting
5. Why are roundness and wall thickness important for PE roll core tubes?
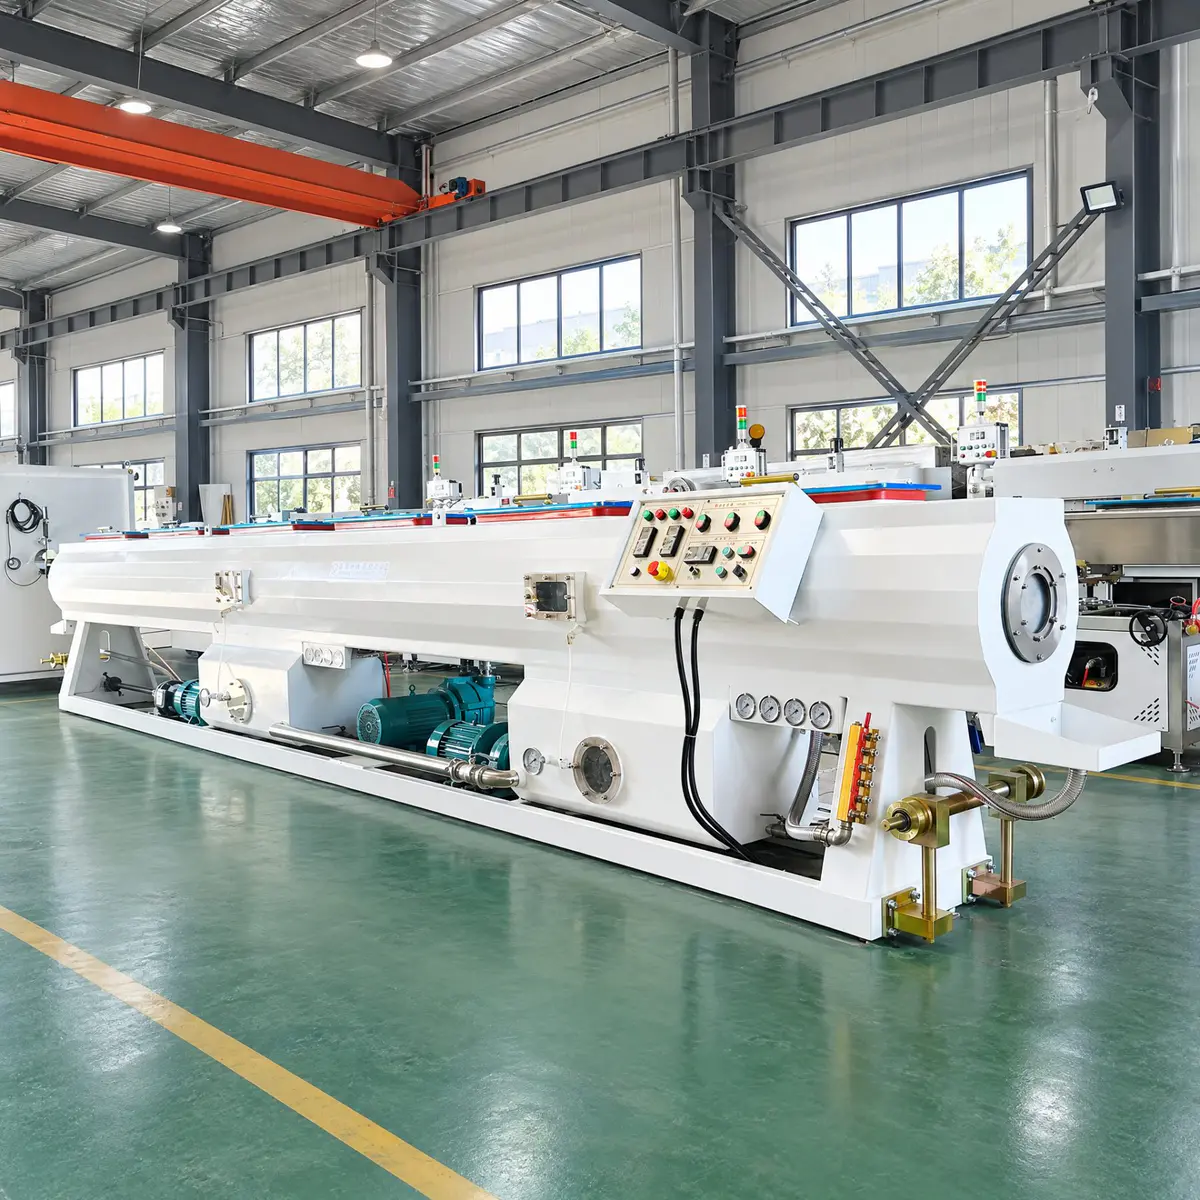
Roundness and wall thickness stability directly affect winding quality, roll balance, and the final use of the PE core pipe.
PE core pipes are not only simple plastic tubes. They work as the structural center of roll materials. If the pipe is not round enough, or if the wall thickness changes too much, it can cause problems during winding and storage.
Common problems caused by unstable pipe dimensions include:
- Uneven roll winding
- Core deformation under pressure
- Poor roll balance
- Difficulty fitting shafts or winding equipment
- Reduced load-bearing performance
This is why QTech-Machinery focuses on the following points in the line design:
| Key Point | Why It Matters |
|---|---|
| Stable PE plasticizing | Reduces melt fluctuation |
| Customized mould design | Helps achieve target pipe size |
| Vacuum calibration | Improves roundness and shape control |
| Spray cooling | Stabilizes pipe dimensions |
| Servo haul-off | Helps maintain constant traction |
| Encoder cutting | Supports accurate pipe length |
According to extrusion troubleshooting references, if pipe weight per meter or wall thickness changes while haul-off speed remains stable, the cause may be related to material feeding or extruder output. If output is stable but pipe dimensions change, downstream calibration, cooling, or traction may need to be checked. [2]
6. How should customers choose the right PE core pipe extrusion line?
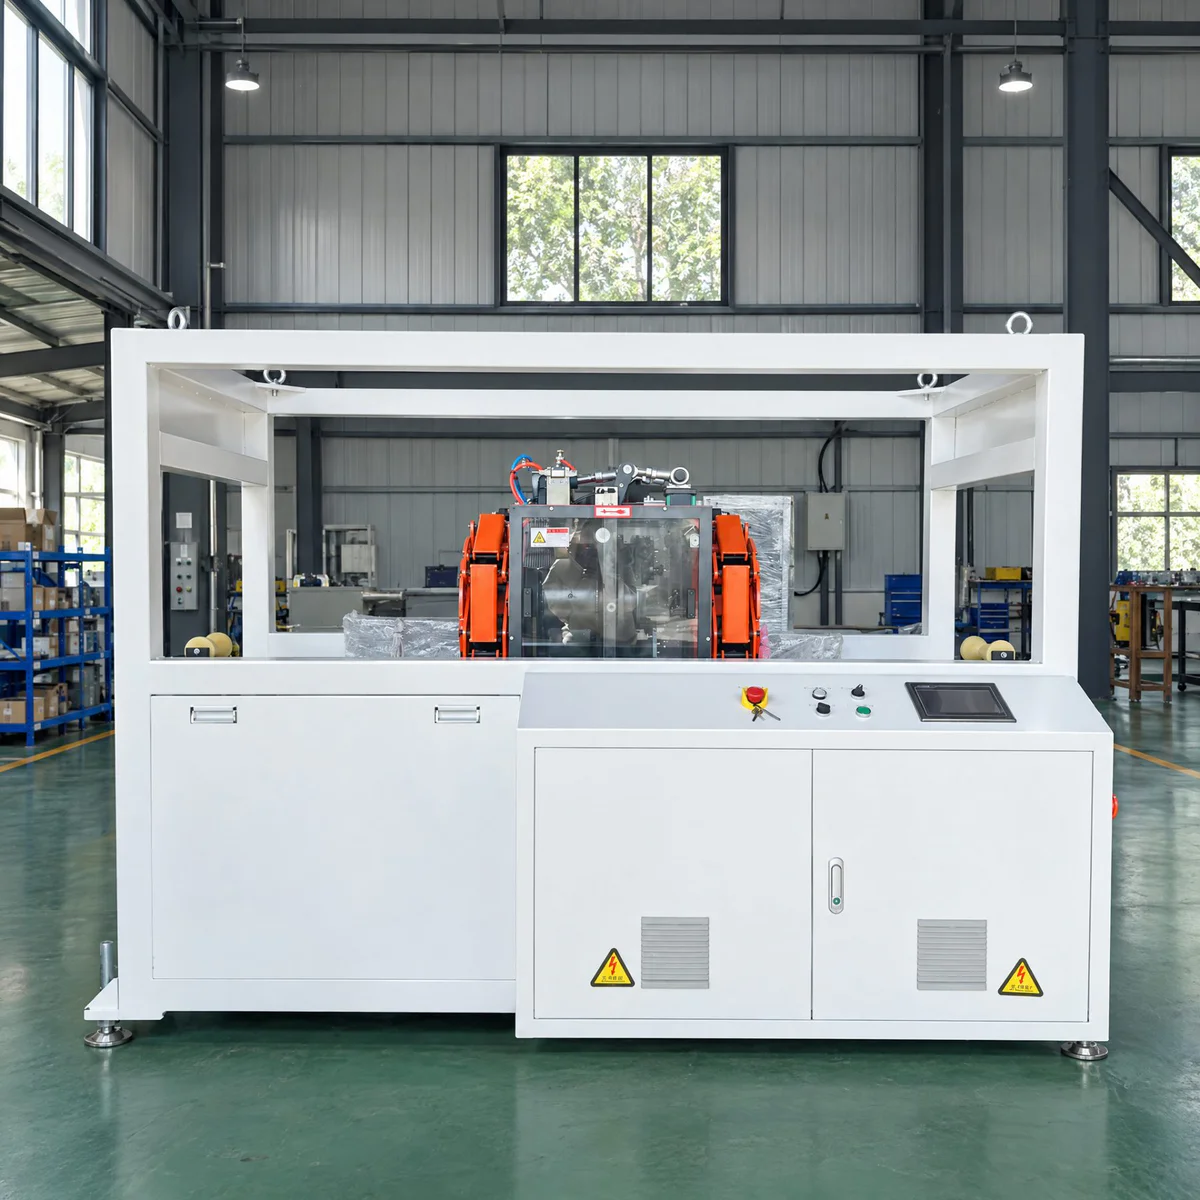
Customers should choose the line according to pipe size, wall thickness, output demand, cutting accuracy, material type, and factory layout.
Before buying a PE core pipe extrusion line, customers should not only ask for the machine price. They should first confirm their product and production requirements.
Customer selection steps
| Step | What to Confirm | Example |
|---|---|---|
| 1 | Product application | Film roll core, foil roll core, packaging roll core |
| 2 | Material | PE or HDPE |
| 3 | Pipe inner diameter | Around 77 mm in this case |
| 4 | Wall thickness | 6 mm, 7 mm, 8 mm, 9 mm, 10 mm |
| 5 | Pipe length | Fixed length according to customer roll size |
| 6 | Output requirement | Daily or hourly production target |
| 7 | Cutting quality | Chipless cutting or saw cutting |
| 8 | Automation level | PLC/HMI, encoder measuring, automatic cutting |
| 9 | Factory layout | Straight-line layout and center height |
| 10 | Service support | Installation guidance, technical documents, spare parts |
For thick-wall PE core tubes, customers should pay special attention to:
- Extruder output stability
- Mould design accuracy
- Vacuum calibration length
- Haul-off force
- Cutting accuracy
- Electrical and control system reliability
QTech-Machinery can recommend a suitable configuration according to the buyer’s required pipe size, material, output, and factory space.
7. What advantages does QTech-Machinery offer for PE core pipe production?
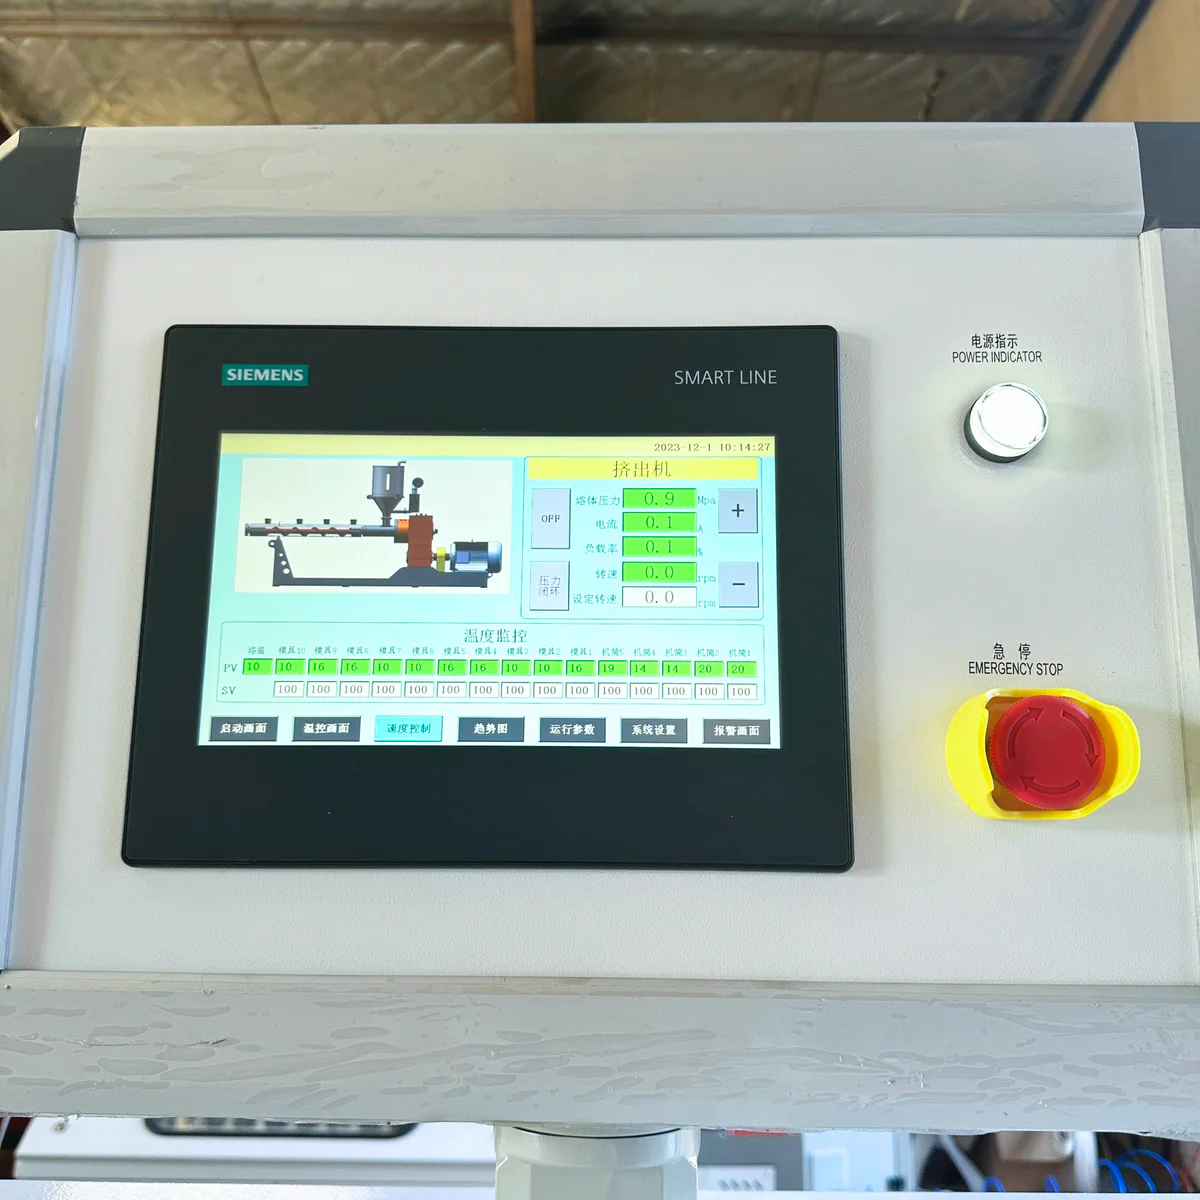
QTech-Machinery provides customized PE core pipe extrusion lines with stable extrusion, matched downstream equipment, servo traction, encoder measuring, and chipless cutting.
In the customer case, QTech-Machinery supplied a complete line rather than only a single machine. This is important because PE core pipe quality depends on the coordination of the whole production process.
QTech-Machinery advantages
| Advantage | Practical Value for Customer |
|---|---|
| Complete line solution | One supplier for extrusion, sizing, hauling, measuring, and cutting |
| Customized mould | Designed for specific pipe ID and wall thickness |
| SJ75/33 extruder | Suitable for stable PE core tube production |
| 9 m vacuum calibration tank | Supports pipe sizing and cooling |
| Three-claw servo haul-off | Helps maintain stable traction |
| Encoder length measuring | Improves fixed-length cutting accuracy |
| Chipless cutting | Reduces chips and improves pipe-end quality |
| PLC/HMI control | Easier parameter setting and operation |
| Industrial electrical components | Supports long-term production reliability |
| Case-based engineering | Configuration based on real customer projects |
The supplied customer case used:
- SJ75/33 single screw extruder
- Customized PE core pipe mould
- 160 vacuum calibration tank
- Three-claw haul-off machine
- Encoder length measuring
- 160 chipless cutting machine
This integrated design helps customers build a practical PE winding core pipe production system for continuous operation.
8. What should customers prepare before requesting a quotation?
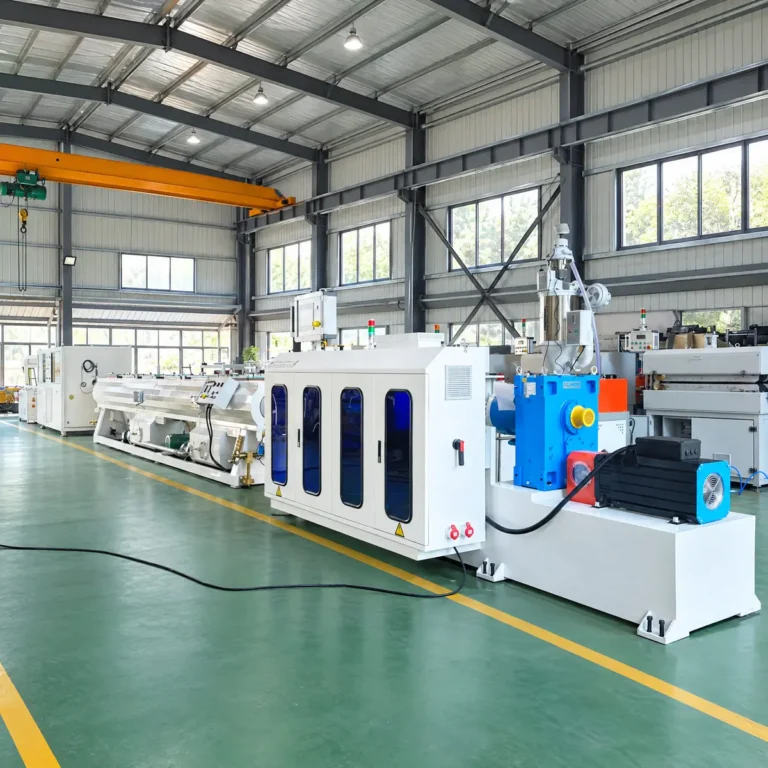
 for PE core pipe extrusion line](https://qinxmachinery.com/wp-content/uploads/2026/11/pe-core-pipe-extrusion-line-extruder-electrical-system-detail-view.webp)
Customers should provide pipe size, wall thickness, material, output requirement, cutting length, power standard, and factory layout information.
To provide an accurate configuration and quotation, the manufacturer needs clear production information from the customer.
Information customers should provide
| Required Information | Example |
|---|---|
| Product name | PE core pipe / PE roll core tube |
| Material | PE / HDPE |
| Pipe inner diameter | Around 77 mm |
| Wall thickness | 6–10 mm |
| Pipe length | Customer-defined fixed length |
| Required output | kg/h or pieces/day |
| Cutting requirement | Chipless cutting |
| Power supply | Voltage, phase, frequency |
| Factory layout | Available length and width |
| Automation requirement | PLC, HMI, encoder, automatic cutting |
Documents QTech-Machinery can provide
| Document | Purpose |
|---|---|
| Technical proposal | Shows recommended machine configuration |
| Quotation | Provides price and commercial terms |
| Layout drawing | Helps customer plan factory space |
| Machine configuration list | Confirms equipment details |
| Electrical configuration list | Shows PLC, HMI, inverter, and electrical parts |
| Process flow description | Explains production steps |
| Product size reference | Helps confirm pipe range |
| Operation guidance | Supports daily production use |
| Spare parts list | Helps future maintenance planning |
| Case reference | Shows similar project experience |
Product List QTech-Machinery Can Provide
QTech-Machinery can provide the following equipment for PE core pipe and related pipe extrusion projects:
| Product / Equipment | Application |
|---|---|
| PE Core Pipe Extrusion Line | PE roll core tube and winding core pipe production |
| HDPE Pipe Extrusion Line | Water supply, drainage, industrial pipe production |
| Single Screw Extruder | PE, PP, HDPE plasticizing and extrusion |
| Pipe Extrusion Die Head | Pipe forming |
| Vacuum Calibration Tank | Pipe sizing and cooling |
| Spray Cooling Tank | Additional pipe cooling |
| Haul-Off Machine | Continuous pipe traction |
| Encoder Measuring System | Pipe length measuring |
| Chipless Cutting Machine | Clean fixed-length cutting |
| Pipe Stacker or Receiving Table | Finished pipe collection |
| Dosing and Feeding Equipment | Material feeding and mixing |
For the detailed customer case, see:
PE Core Pipe Extrusion Line for Roll Core Tube Manufacturing
Practical Configuration Table for This PE Core Pipe Case
| Parameter | Value | Notes |
|---|---|---|
| Line Type | PE Core Pipe Extrusion Line | For PE roll core tube production |
| Material | PE / HDPE | Based on customer product requirement |
| Main Extruder | SJ75/33 Single Screw Extruder | Main plasticizing unit |
| Screw Diameter | 75 mm | Suitable for medium PE core pipe production |
| L/D Ratio | 33:1 | Supports stable plasticizing |
| Main Motor Power | 45 kW | Provides extrusion torque |
| Product Inner Diameter | Around 77 mm | Customer case specification |
| Wall Thickness | 6 / 7 / 8 / 9 / 10 mm | Multiple product options |
| Mould | Customized PE Core Pipe Mould | Designed according to pipe size |
| Vacuum Tank | 160 Vacuum Calibration Tank | For sizing and cooling |
| Vacuum Tank Length | 9 m | Supports cooling and calibration |
| Vacuum Range | 0.02–0.08 MPa | For pipe shape control |
| Haul-Off Type | Three-Claw Haul-Off | Stable traction for thick-wall pipe |
| Haul-Off Speed | 0.2–3 m/min | Adjustable production speed |
| Drive System | 3 × 1.5 kW Servo Motors | Servo traction control |
| Cutting Machine | 160 Chipless Cutter | Automatic fixed-length cutting |
| Cutting Range | 50–160 mm | Suitable for this pipe range |
| Measuring Method | Encoder Meter Counting | Sends cutting signal |
| Control System | PLC + Touch Screen | Convenient operation |
External References and Industry Notes
The following external resources are useful for understanding general plastic pipe extrusion control and troubleshooting:
-
Online Controls discusses pipe extrusion OD, wall thickness, and ovality control, mentioning the importance of vacuum repeatability, cooling uniformity, and haul-off stability in pipe sizing. [0]
Source: https://www.onlinecontrols.com/feeds/blog/ultra-precision-control-systems -
Wanplas explains that traction speed instability in plastic pipe extrusion can affect pipe wall thickness and production stability. [1]
Source: https://www.wanplas.com/industry-blogs/plastic-pipe-extrusion-line-traction-speed-instability-problems-and-drive-system-maintenance/ -
MIDTECH notes that changes in pipe weight per meter, haul-off speed, material feeding, and extruder output should be checked when pipe wall thickness moves out of tolerance. [2]
Source: https://midtech-mc.com/plastic-pipe-wall-thickness/ -
Gauge Advisor explains that dimensional changes in extrusion may relate not only to melt pressure, but also to cooling, vacuum sizing, internal air pressure, and puller or haul-off speed. [3]
Source: https://gaugeadvisor.com/what-causes-extrusion-pressure-fluctuations/
These references support a practical point: good PE core pipe production depends on the full system, not only the extruder. For roll core tube applications, the extrusion line should coordinate material melting, mould forming, vacuum calibration, cooling, stable hauling, length measuring, and accurate cutting.
Conclusion
A PE core pipe extrusion line is used to produce strong and dimensionally stable PE roll core tubes for film, foil, packaging, electronic material, and other industrial winding applications.
For customers who need PE core pipes with good roundness, stable wall thickness, accurate length, and clean pipe ends, QTech-Machinery can provide a complete customized solution from extrusion to chipless cutting.
The customer case shows a practical configuration with an SJ75/33 single screw extruder, customized PE core pipe mould, 160 vacuum calibration tank, three-claw haul-off, encoder length measuring, and 160 chipless cutting machine. This makes it a useful reference for buyers planning a similar PE roll core tube production line.
For a similar project, customers can prepare their pipe diameter, wall thickness, material, required length, output target, and factory layout, then request a customized configuration from QTech-Machinery.