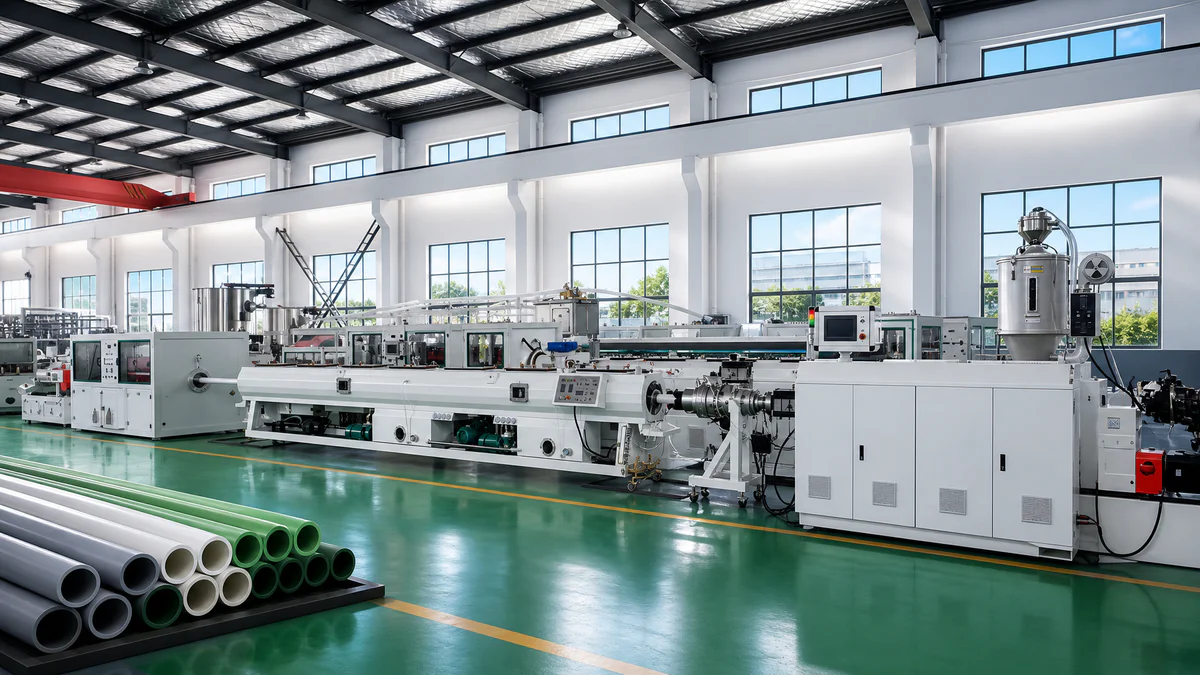
China PPR Pipe Extrusion Line Factory
Complete PP-R pipe lines from 16mm to 160mm, as single layer, three layer or glass fiber reinforced builds. Every machine, from the dosing unit to the stacker, is sized around the pipe you sell, the output you need and the plant it goes into, then the whole line runs on your specification before it leaves Zhangjiagang.
- 16mm to 160mm pipe range
- Single, three layer and glass fiber
- Full run test before shipment
- CE, ISO 9001 and SGS
16mm To 160mm
Hot and cold water pipe sizes, with die tooling and a calibration sleeve for each size you run.
Single, Three Layer, Glass Fiber
Co-extruders and a multilayer die head join the line when the pipe wall has more than one layer.
Stripe, Print, Cut, Stack
Colour stripes and online printing as options, then cutting and stacking at the end of the line.
Plan Your PPR Line Machine By Machine
Start wherever your question sits: the pipe structure you make, what each station on the line does, the numbers from a line we built, or what to send for a quotation.
Pipe Structures
Single, three layer, glass fiber
Line Flow
Ten stations, hopper to stacker
Reference Build
A 20 to 110mm line in numbers
Extrusion And Layers
Screw, co-extruders, die, dosing
OD And Weight Control
Calibration, cooling, haul-off
Marking And Cutting
Stripes, printing, pipe ends
Lengths, Coils, Bundles
What leaves the line
Quality Checks
What buyers measure
Project Steps
From spec to start-up
FAQ
Sizes, layers, cutting, testing
Send Your Details
Inquiry form for Maggie
Single Layer, Three Layer Or Glass Fiber Reinforced
The structure of the pipe wall is the first decision, because it fixes how many extruders the line carries and how much work the die head does. Find the column that matches your product today, or the one you plan to add next.
Single Layer PP-R
What The Line Needs
One single screw extruder, a PP-R die head, vacuum calibration, spray cooling, a haul-off, a cutter and a stacker. A small co-extruder is added only when you want colour stripes on the pipe.
What We Confirm
Size range, wall or pressure grade, output for each size, stripe colours.
Three Layer PP-R
What The Line Needs
Every layer gets its own extruder and its own speed control, and the melt streams meet inside a multilayer die head. That head is laid out around the material, thickness and ratio you specify for each layer.
What We Confirm
Layer order, material and target thickness of each layer, output of every extruder.
Glass Fiber Reinforced PP-R
What The Line Needs
A three layer build in which one co-extruder runs the glass fiber compound. Glass fiber is abrasive, so the screw and barrel on that extruder are specified for wear, and layer structure and bonding are reviewed before the die is drawn.
What We Confirm
Which layer carries the fiber, compound grade, bonding check, spare wear parts for that extruder.
If a three layer or reinforced product is on next year's plan, put it in your first inquiry. Room for extra melt channels and stripe feeds costs little on a drawing and a lot once the die head has been machined.
Once you know how many layers the pipe wall carries, every station after the hopper can be sized to it, and the next section walks through them in order.
Ten Stations From Hopper To Stacker
A PP-R line reads left to right. Two stations are optional and shown with a dashed edge; the other eight make up the standard PP-R flow. Each card links to the machine page with its sizes and options.
Dosing And Feeding
Meters PP-R resin and a small share of masterbatch into the hopper at the ratio your recipe sets, so colour does not drift between batches.
Dosing EquipmentSingle Screw Extruder
Melts and homogenises the resin. Screw size follows the kg/h your heaviest pipe needs, not the largest diameter on the list.
ExtrudersCo-Extruders
One small extruder per stripe colour or per extra layer, each with its own speed control. Three layer and glass fiber pipe need them.
Co-ExtrudersPPR Die Head
Forms the tube and, on multilayer pipe, joins the melt streams in the order and ratio you specify.
Die HeadsVacuum Calibration Tank
A sizing sleeve and controlled vacuum fix the outside diameter while the pipe is still soft.
Vacuum TanksSpray Cooling Tank
Keeps drawing heat out until the wall is stable enough to grip, print on and cut.
Spray Cooling TanksHaul-Off
Pulls at a steady speed. A steady pull gives a steady wall, and a steady wall gives a steady pipe weight.
Haul-Off MachinesOnline Printer
Marks your brand and product text on the cooled pipe surface as it passes.
Pipe Cutter
Travels with the pipe and cuts it to length. Chipless knife cutting is often considered for suitable PP-R sizes.
Cutting MachinesStacker Or Winder
Collects straight lengths for bundling, or coils a size your market buys on reels where the pipe allows it.
Weighing PP-R against HDPE, PVC or MPP? Our pipe extrusion lines overview sets every line family side by side.
A flow chart is easy to agree with, so the next section shows a PP-R line we actually built, with the screw, motor, tank and haul-off figures written out.
One PP-R Line, Written Out In Numbers
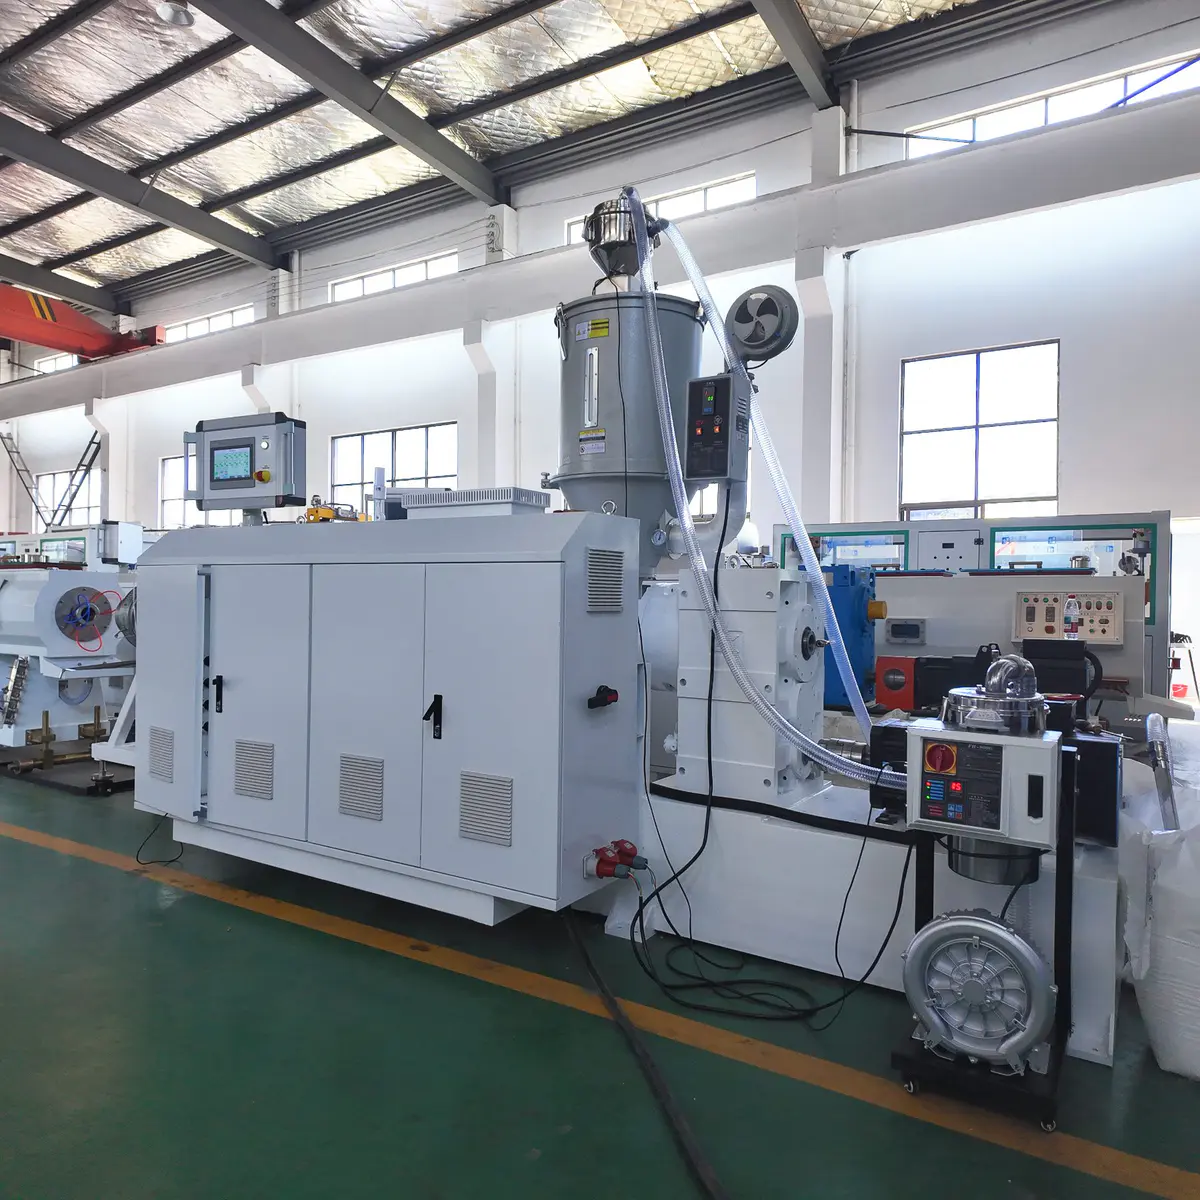
This line was configured for a plumbing pipe producer making PP and PP-R pipe from 20mm to 110mm. Read it as a checklist for any quote: every row is a figure you can ask a supplier to state.
| Station | Reference Configuration |
|---|---|
| Pipe And Material | PP and PP-R pipe, 20mm to 110mm |
| Main Extruder | SJ75/33 single screw, 75mm screw, 33:1 L/D, BM type screw |
| Drive | 55 kW main motor, Yaskawa inverter speed control |
| Barrel Heating | Ceramic heaters, 6 zones of 4.5 kW, fan cooling |
| Colour Marking | SJ25/25 marking extruder |
| Vacuum Calibration | 6 m stainless steel tank, two 4 kW vacuum pumps |
| Spray Cooling | 6 m tank, 5.5 kW water pump |
| Haul-Off | Three-jaw caterpillar, 2500 mm effective length, 0.2 to 15 m/min |
| Cutting | No-chip cutter for 20mm to 110mm pipe |
| Electrical | Siemens and Schneider components |
A reference, not a catalogue model. Your configuration is drawn from your own sizes, materials and output, and any row can change.
Scaling It To Your Range
- Toward 16mm: small pipe runs fast, so haul-off and cutter speed lead the selection, and a belt haul-off is worth comparing with caterpillars.
- Toward 160mm: large pipe runs slower and needs more cooling length, and the haul-off needs more contact on the pipe.
- More sizes: each size you add brings its own die tooling and calibration sleeve.
- More output: the extruder is sized to the kg/h of your heaviest pipe, not to the widest diameter alone.
Every row in that table depends on melt quality, which is why the next section opens at the screw, the co-extruders and the die.
Screw, Co-Extruders, Die Head And Dosing
Four parts of the line decide whether the melt reaching the calibration tank is even, coloured correctly and split between layers in the right ratio. Pick one to see its job on a PP-R line and what we confirm before sizing it.

A Single Screw Sized To Your Heaviest Pipe
PP-R is a polyolefin, and for polyolefin pipe a single screw extruder is the usual starting point. Our single screw machines run from 45mm to 120mm screw diameter. Which one you get depends on the resin, the kg/h your heaviest size needs and the hours you run. The reference line used a 75mm screw at 33:1 L/D with six fan-cooled ceramic heating zones.
We Confirm
- Resin grade, PP-R or PP-RCT
- Required kg/h for each size
- Recycled content, if any
- Voltage and frequency
A Separate Melt Stream For Each Stripe Or Layer
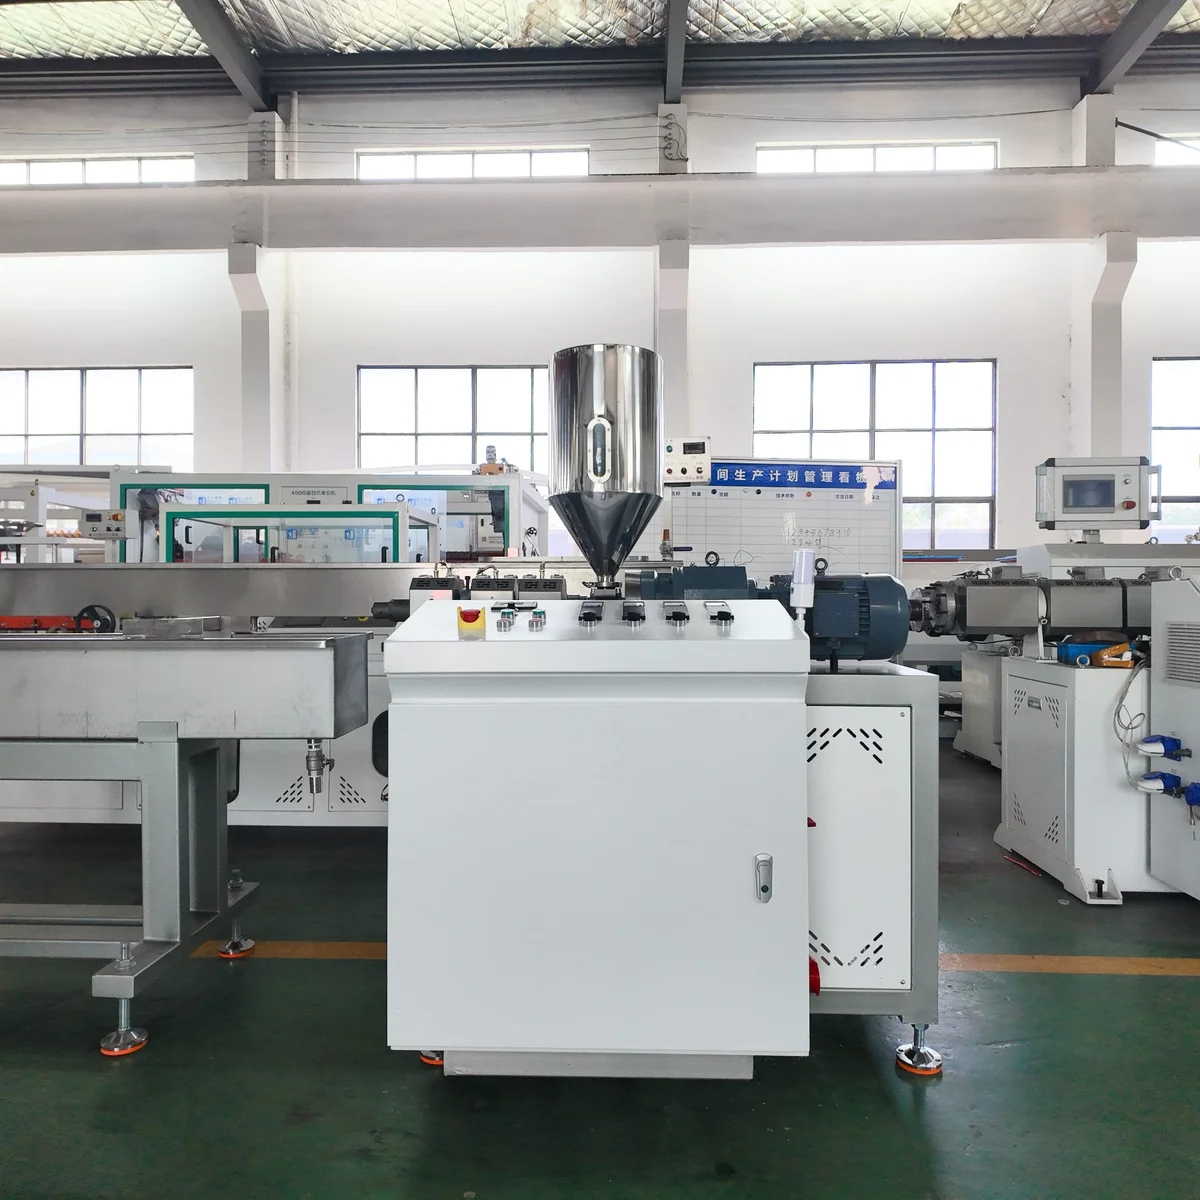
A co-extruder feeds its own material under its own speed control, so a stripe colour or an extra layer can be trimmed without touching the main extruder. For stripes it is a small machine; the reference line ran an SJ25/25 for colour marking. For a full inner or outer layer, or a glass fiber layer, it is sized to that layer's thickness at your line speed, and on glass fiber compound its screw and barrel are specified for wear.
We Confirm
- Number of stripe colours
- Which layer each extruder feeds
- Layer thickness at each size
- Glass fiber compound grade
Layers Meet Inside The Die, In The Ratio You Set
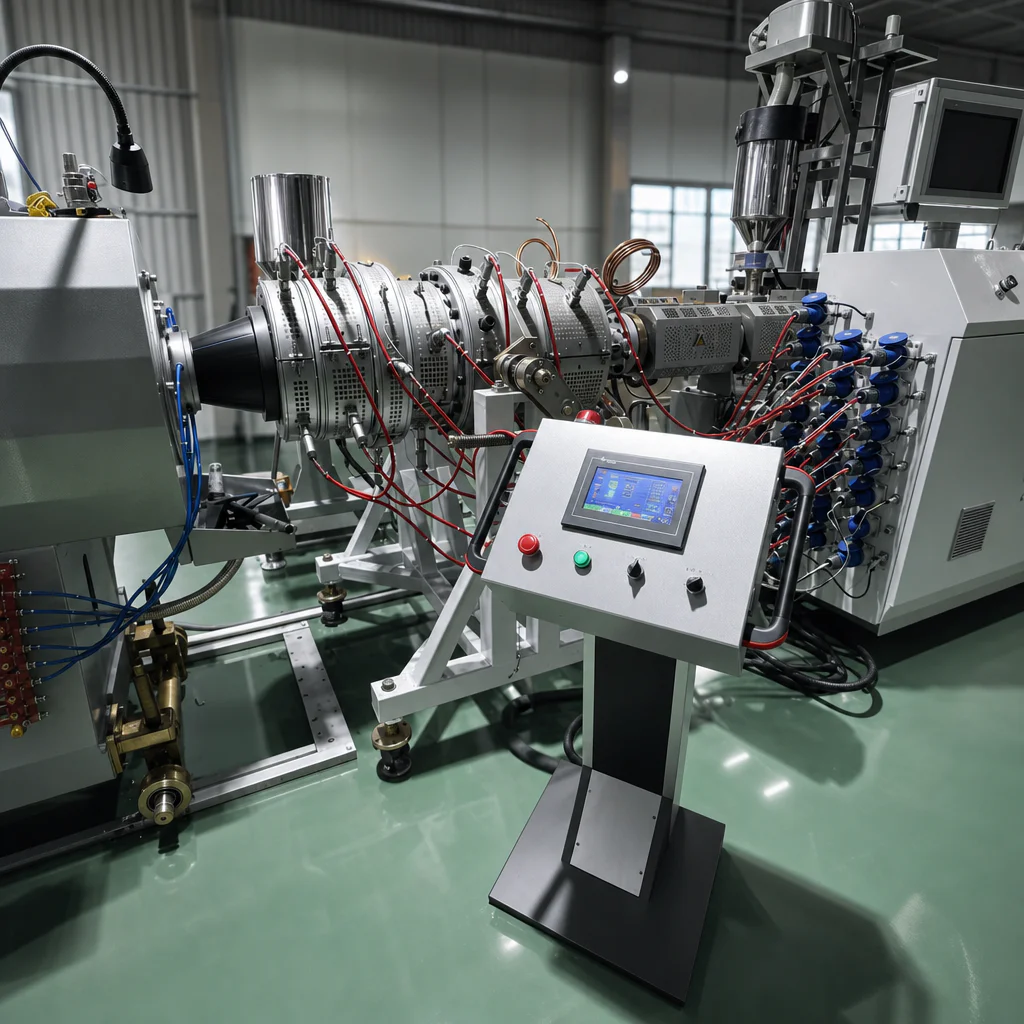
On PP-R the die shows its quality on the pipe surface: melt has to reach the land evenly all the way round, at every size you switch to during the week. A multilayer head adds an inlet and a channel per layer, designed around layer count, each layer's material and target ratio, pipe dimensions and the output of every extruder feeding it. The final split is only as steady as those extruders, so the whole co-extrusion setup is reviewed together, and you approve the head drawing before machining.
We Confirm
- Layer count and order
- Material and ratio per layer
- Stripe count and position
- Main and co-extruder outputs

Short Recipes, Small Additions, Tight Dosing
A PP-R recipe is usually short: resin, a colour masterbatch at one or two percent, perhaps a functional additive. Because the additions are so small, the dosing unit decides whether this week's green matches last month's. Gravimetric dosing holds kg/h by weight; volumetric suits stable pellets with moderate accuracy needs. Keep the resin clean and dry as well: moisture, contamination or a drifting melt flow index shows up as bubbles, surface marks and uneven wall.
We Confirm
- Resin and masterbatch grades
- Addition ratios
- Regrind share, if any
- Number of extruders to feed
Even melt still leaves the die soft, so outside diameter and weight per metre are only settled in the sizing and pulling section that comes next.
Where Outside Diameter And Pipe Weight Get Fixed
Three machines after the die hold the numbers buyers measure first. Each one goes wrong in a way you can recognise, which helps when reading a quote and again when troubleshooting a running line.
 Stage 1
Sets The Outside Diameter
Vacuum Calibration
Sleeve and tank work as one sizing system. Enough vacuum holds the soft pipe against the sleeve; too much adds friction and leaves drag marks on the surface. The tank is sized to your size range, wall, line speed and the sleeve set for each size.
Reference line: 6 m stainless tank with two 4 kW vacuum pumps.
 Stage 2
Locks The Shape In
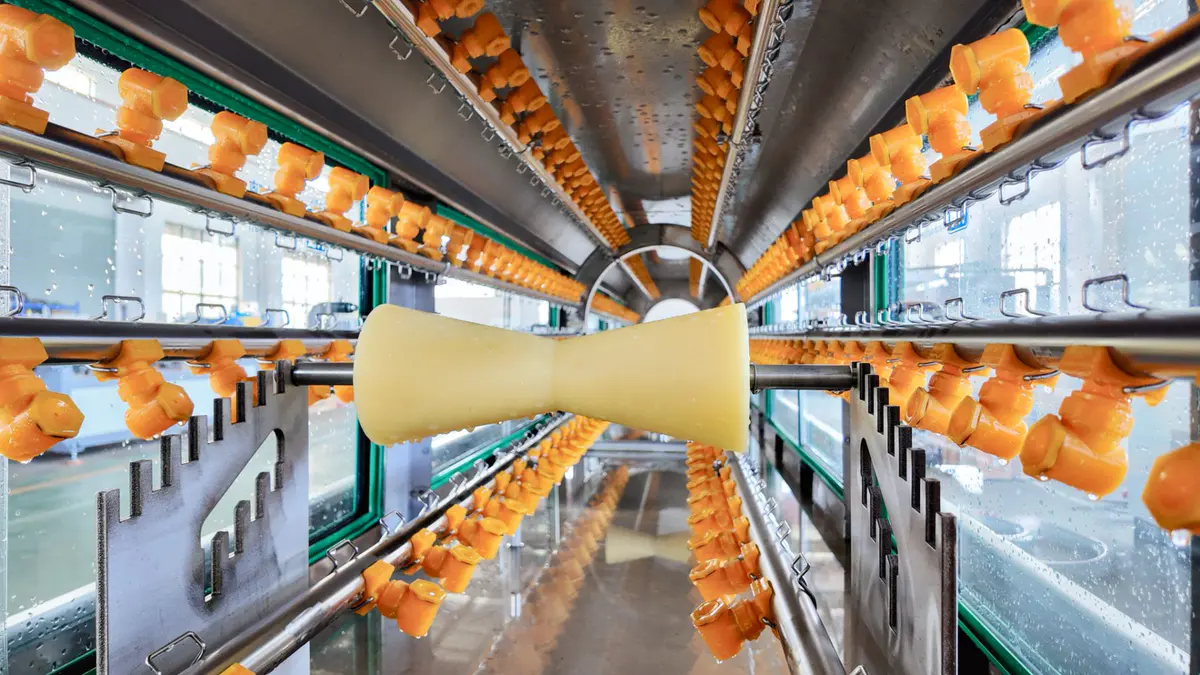
Spray Cooling
Nozzles have to wet the whole circumference evenly. Water bunched on a few zones cools one side first, and the pipe carries that forward as ovality or uneven wall. Tank length comes from diameter, wall, line speed, water temperature and any cooling already on the line.
Reference line: 6 m tank with a 5.5 kW water pump.
 Stage 3
Sets Wall And Weight Per Metre
Haul-Off Speed
At a fixed extruder output, pulling speed decides the wall, so a haul-off that wanders under load shows up as weight drift. Every track has to run in step with the others and grip without marking or flattening the pipe.
Reference line: three-jaw caterpillar, 2500 mm contact length, 0.2 to 15 m/min.
Measure The Pipe At Three Points
Tank Exit
If OD is already wrong here, extra cooling will not correct it. Look at the extruder, the die or the calibration.
After Spray Cooling
Roundness that changes between here and the tank exit points at the spray pattern or the cooling length.
At The Cutter
Weight per metre is the quickest read of wall over a shift. If output and pulling speed hold, weight holds with them.
With diameter and weight held, the last metres of the line decide how the pipe is marked and how cleanly each end is cut.
Stripes, Printing And A Clean Pipe End
These are the details an installer notices first, so they are planned with the rest of the line instead of being added after it is built.
Colour Stripes
A stripe is extruded into the wall, not painted on. It comes from a co-extruder feeding a channel in the die head. Stripes commonly separate hot water from cold water pipe, or mark a product series or a brand.
How many stripes you want and where they sit around the pipe change the die design. The stripe extruder also has to follow the main extruder and the line speed, or the line breaks up and wanders along the pipe.
Online Printing
An optional online printer marks your brand and product text on the pipe after the spray cooling tank, where the surface has settled.
Readable print along the whole length is one of the pipe checks you can add to the run test, next to OD, weight and the cut end.

Cutting And Pipe Ends
PP-R pipe is welded at installation, and a rough or angled end can spoil the weld and the seal. Chipless knife cutting is often considered for suitable PP-R sizes because it cuts without making chips; wall, diameter and cutting cycle are checked before the method is fixed.
The cutter tracks how far the pipe has travelled and moves with it during each cut, so every piece comes off at the length set on the screen. Knives are wear parts: a dull edge shows up on the pipe end before any alarm does.
Reference line: no-chip cutter, 20mm to 110mm.
View CuttersCut lengths, coils and bundles are handled in different ways, and your choice changes the last machines on the line.
What Leaves The Line, And In What Form
The standard PP-R flow finishes with a cutter and a stacker. Coiling and bundling are added where your market or your warehouse asks for them.

Straight Lengths
The stacker takes each cut length, supports it along its whole length and tips it into the collection area before the next piece arrives. Tell us your cut lengths, such as 3 m, 4 m or 6 m, your heaviest pipe and the cutting cycle at your smallest size.
Pipe Stackers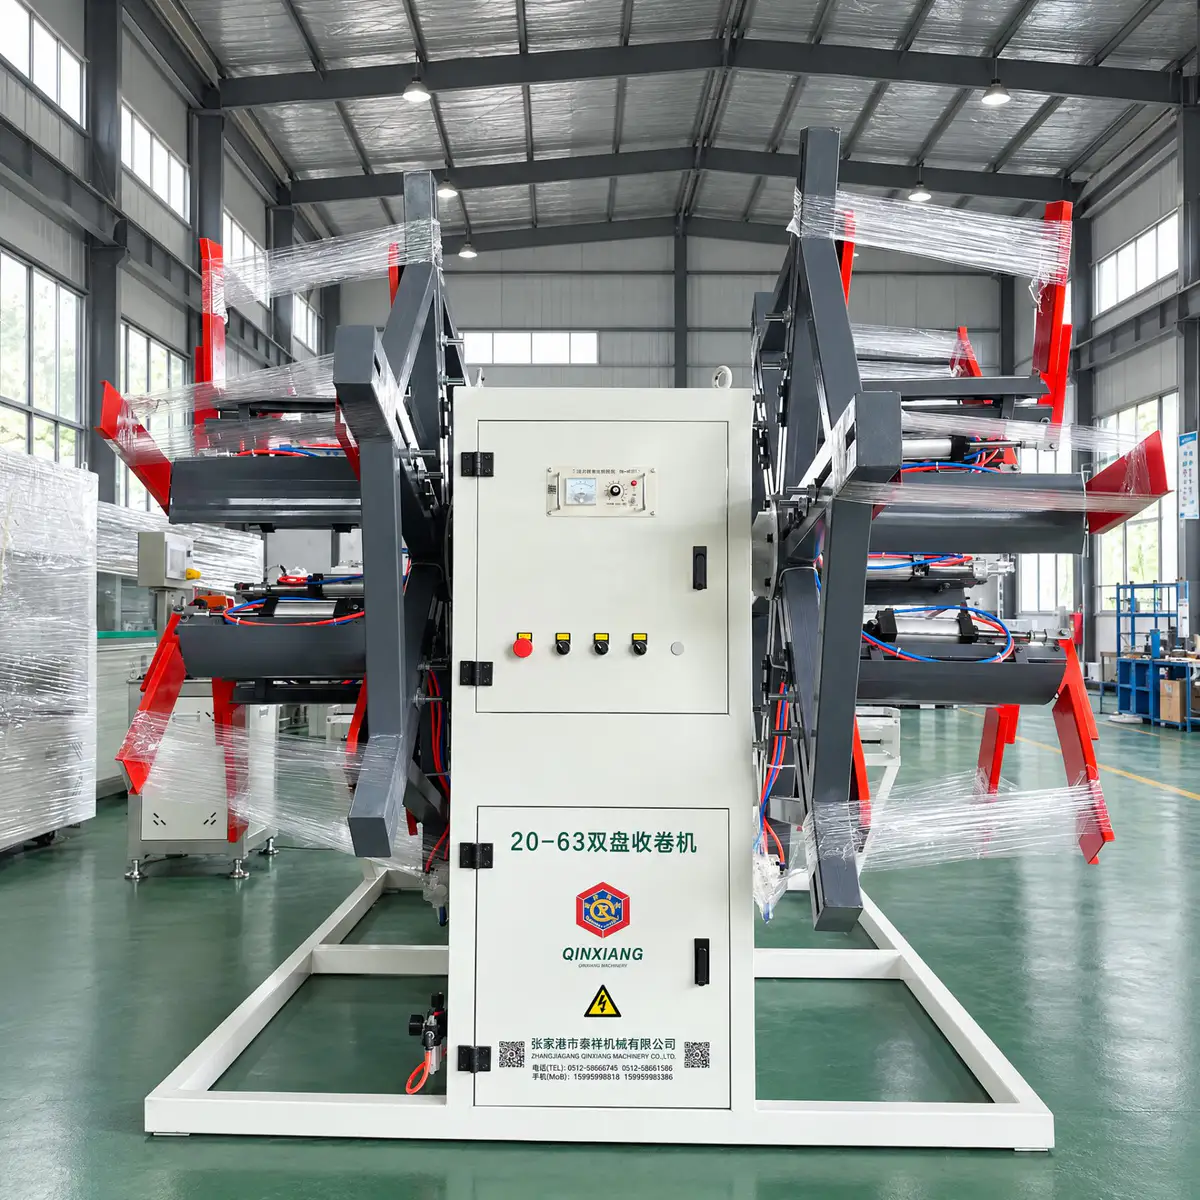
Coils
Our coilers are built for flexible pipe such as PE-RT and PEX. Whether a small PP-R size can go on a reel depends on how stiff the pipe is and how its wall is built, so we review it before a winder goes into the quote. Where it fits, tension control keeps thin walls from going oval.
Pipe WindersBundles
Packaging machines count the pipes, form the bundle and hold it with strap, film or a bag. Pipes per bundle and bundle shape size the machine, and PP-R wall stiffness changes how the pipes settle into the stack.
- Pipes per bundle at each size
- Bundle shape and weight
- Strap, film or bag
- Bundles per hour at full line speed
A photo of the bundle you ship today answers most of these at once.
Pipe Packaging MachinesEvery station on this page serves a short list of checks your buyers run on the finished pipe, and that list is next.
Eight Checks A PP-R Buyer Runs On Your Pipe
Your local pipe standard sets the tolerances. The table shows which part of the line holds each check, so you know which question to ask about every machine in a quote.
01OD Tolerance
What it tells your buyerThe pipe fits the fittings it will be welded into
Where the line holds itCalibration sleeve, vacuum level, cooling
02Roundness
What it tells your buyerThe pipe kept its shape through cooling and pulling
Where the line holds itEven spray pattern, haul-off grip, cooling length
03Pipe Weight
What it tells your buyerThe wall stayed consistent over the shift
Where the line holds itSteady extruder output, steady haul-off speed
04Surface Gloss
What it tells your buyerHow the pipe looks on a distributor's shelf
Where the line holds itDie flow and land, clean dry resin, calibration friction
05Colour Match
What it tells your buyerOne batch looks like the next
Where the line holds itMasterbatch dosing accuracy
06Layer Bonding
What it tells your buyerThree layer and glass fiber walls act as one wall
Where the line holds itMultilayer die layout, balanced extruder outputs
07Cut End
What it tells your buyerA square, clean end that is ready to weld
Where the line holds itCutting method, knife condition, cutter tracking
08Printing
What it tells your buyerThe marking can be read along the whole length
Where the line holds itPrinter after cooling, steady line speed
What Gets Written Down Before Shipment
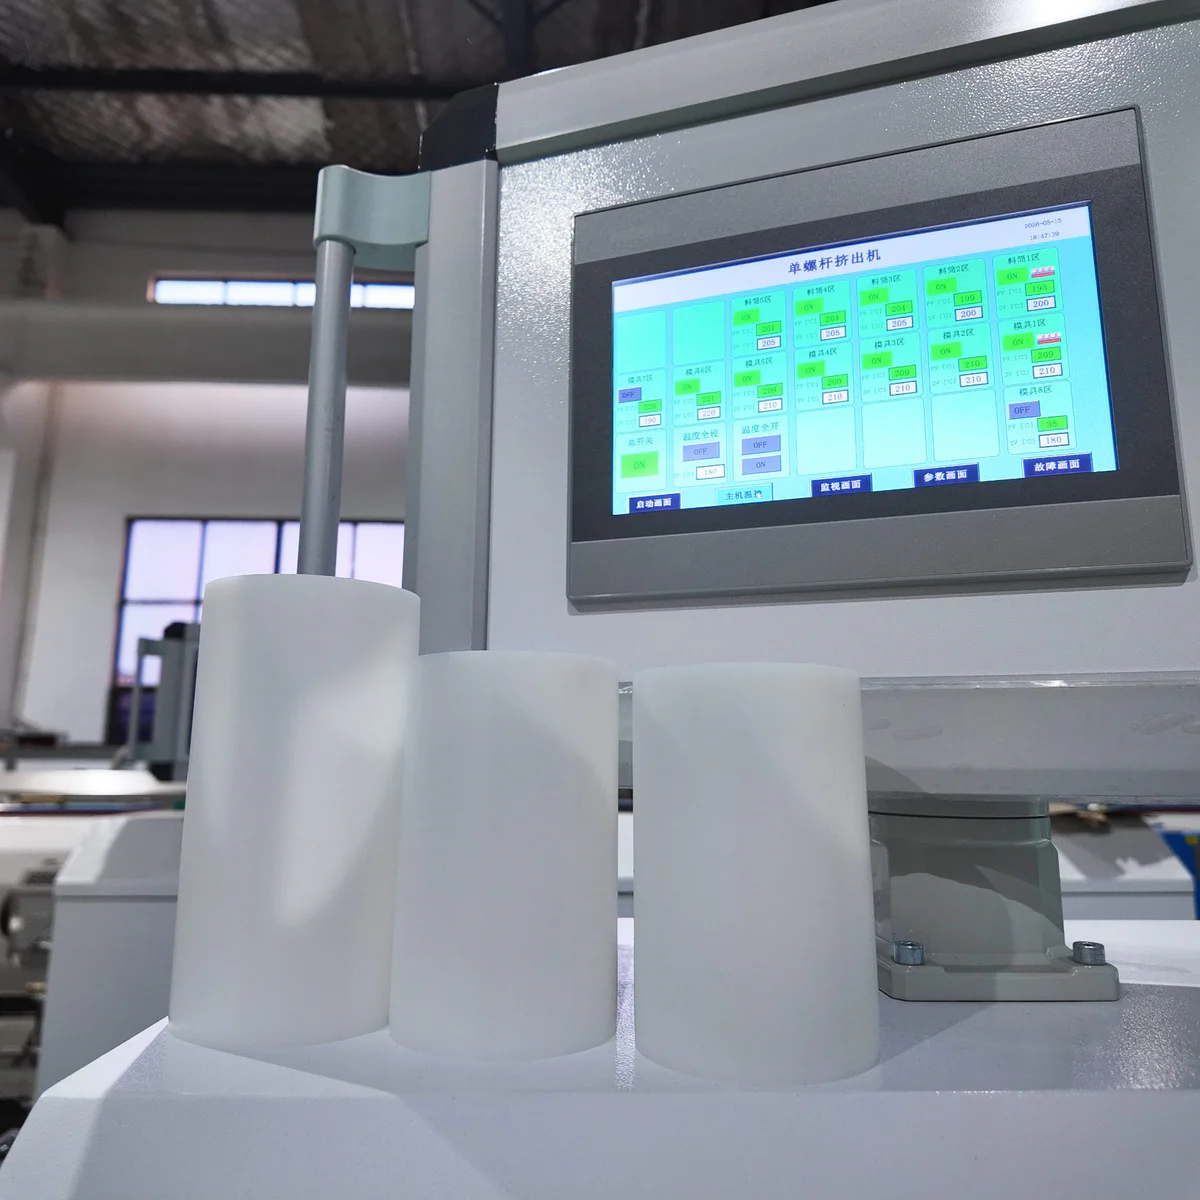
Every line runs before it ships and the readings are recorded. Where material testing is part of the agreed scope, the record covers:
- Actual output
- Screw speed
- Motor load
- Melt temperature
- Melt pressure
- Continuous running time
Checks on the finished pipe from the table above, sample pipe, photos or a running video are added as your project needs them.
Those checks feed the run test, which is step four of how a PP-R line goes from your first message to steady production.
From Your Pipe Spec To A Running Line
Six steps, and each one ends with something you can check before the next one starts.
Send These For A First Configuration
- Application: hot and cold water, plumbing or industrial
- Size range within 16mm to 160mm
- Wall, SDR or pressure grade, and your pipe standard
- Single layer, three layer or glass fiber
- PP-R or PP-RCT grade, masterbatch, additives
- Stripe colours and printing
- Output per size in kg/h or m/min
- Voltage, frequency and workshop length
- Straight lengths, coils or bundles
Missing a few? Send what you have and Maggie asks for the rest.
Requirement Review
We read your spec and come back with questions on anything that would change the machine list.
Configuration And Drawings
Machine list, layout, power demand and options. You approve the die head drawing before any steel is cut.
Manufacturing
Machining, assembly and cabinet wiring happen under one roof in Zhangjiagang.
Run Test
The line runs before shipment with the readings recorded, plus the pipe checks you agreed.
Packing And Shipment
Export packing, with drawings, the spare parts list and shipping documents.
Installation And Training
Engineer visit, remote start-up support and operator training for your team.
Delivered lines and trial runs are collected on our cases page, and every pipe line family is on the pipe extrusion lines overview.
PPR Pipe Line Questions
Short answers to what PP-R producers ask before they order. If yours is missing, send it to Maggie.
We build PP-R lines across 16mm to 160mm, but one line is normally set up for a band inside that range. Small pipe runs fast while large pipe needs slower speed and more cooling length, so a very wide band pulls the extruder, tanks and haul-off in opposite directions. Each size also needs its own die tooling and calibration sleeve. Send the sizes you sell and we will tell you whether one line or two makes more sense.
Co-extruders join the main extruder, and the single layer die is replaced by a multilayer head that brings the melt streams together. The head is designed around each layer's material and target thickness, and the extruders are sized so their outputs stay balanced, because the layer split is only as steady as the machines feeding it.
Yes, as a three layer build in which one co-extruder runs the glass fiber compound. Glass fiber is abrasive, so the screw and barrel on that extruder are specified for wear and the wear parts are listed with the order. Layer structure and bonding are confirmed before the die head is designed.
A single screw extruder is the usual starting point for PP-R and PE-RT. Screw size comes from your resin, the kg/h of your heaviest pipe and your running hours. Our single screw range covers 45mm to 120mm screw diameter; the 20mm to 110mm reference line ran a 75mm screw at 33:1 L/D with a 55 kW main motor.
Yes. Stripes come from a small co-extruder feeding a channel in the die head, so give us the number of stripes and their positions before the head is drawn. An online printer is an option after the spray cooling tank and marks your brand and product text on a settled surface.
Chipless knife cutting is often considered for suitable PP-R sizes because it cuts without chips and leaves a clean end for welding. Wall thickness, diameter and the cutting cycle are reviewed before the method is confirmed. The reference line used a no-chip cutter covering 20mm to 110mm.
The usual PP-R line ends with a cutter and a stacker. Our coilers are built for flexible pipe such as PE-RT and PEX, and whether a small PP-R size can be coiled depends on its stiffness and wall construction. We review that with you before a winder is added to the quote.
Every line gets a full run test before shipment with the readings recorded. Where material testing is in the agreed scope, that record includes the real kg/h, melt temperature and pressure, screw speed, motor load and how long the line ran without stopping. Pipe checks, sample pipe, photos or a running video can be added.
Your size range, wall or pressure grade and pipe standard, the pipe structure, materials, stripe and printing needs, output per size, voltage, and whether pipe leaves as lengths, coils or bundles. A pipe drawing or a sample photo helps. Gaps are fine; Maggie will ask about them.
A stripe or an extra layer needs a channel in the die head, so the easiest route is to plan it from the first drawing. Tell us what you may add in the coming years and we lay out the die and the floor space with that in mind, rather than reworking a finished head.
Get A PPR Line Configuration From Maggie
Tell us the pipe you make, or the one you plan to make. Maggie replies within 24 hours with a machine list built around it and the questions that still need an answer.
Maggie
Pipe Line Sales, QTech Machinery
Replies within 24 hoursMessages from this form come straight to me. Send your sizes and pipe structure, and I come back with a configuration you can compare line by line, along with anything in the plan I expect to cause trouble later.
A size range and a pipe structure are enough to start. QTech Machinery ships extrusion lines to customers in 60+ countries.
Maggie
Sales, Zhangjiagang Qinxiang Machinery Co., Ltd.
Tell Us About Your PP-R Pipe
Fields marked are required.