Quality Control From Part To Pipe
CE, ISO 9001 and SGS, full run test before shipment.
Behind that line sits a chain of checks. Parts are measured before they meet, each machine is aligned and wired against the configuration you approved, and the finished machine runs on our floor before anyone builds a crate around it. The record, the photos and the video come to you while it is still here.
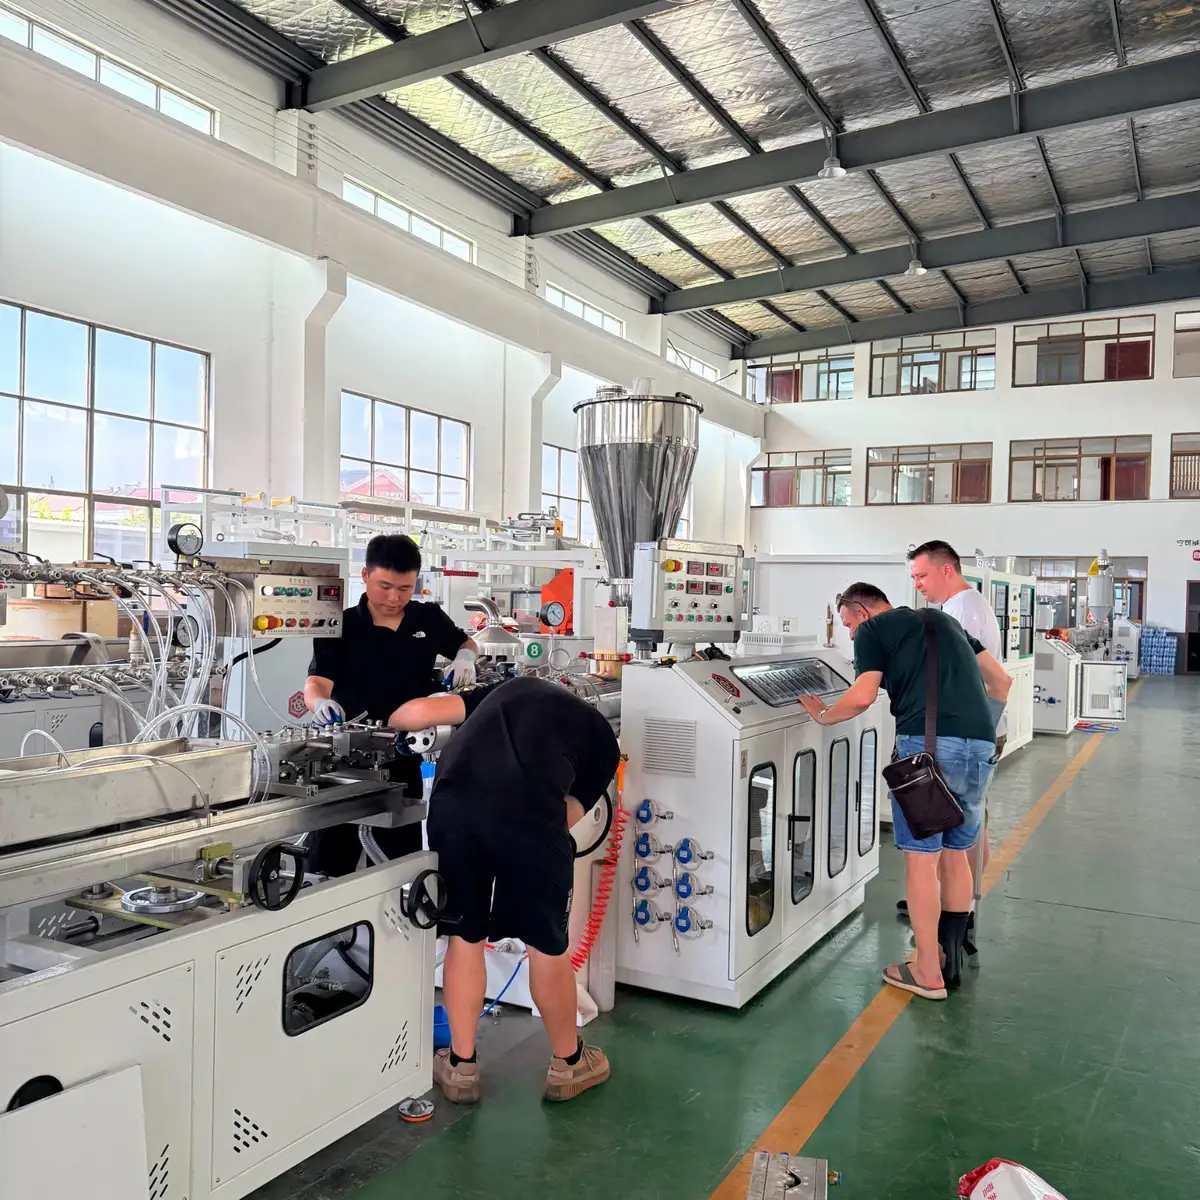
Built in Zhangjiagang, Jiangsu
Checked against your approved configuration before packing.
Certified
CE, ISO 9001, SGS
The marks QTech Machinery works under. Ask Maggie for the CE verification of conformity.
Run Test
Every Machine Runs
Nothing is crated without a running check of drive, heat, controls and alarms.
Your Spec
Pipe You Signed Off
Material trials are judged on the size, wall and surface you approved, where your scope includes one.
Witness
Attend Or Watch
Come in person, join by video call, or send a third-party inspector instead.
Jump To The Check You Need
Eight stages, in the order a machine meets them, from the first measured part to the closed crate. For the workshop itself and the route a machine takes through it, see Our Factory.
Before Assembly
Specs, parts, components
In-Process Checks
Dies, barrels, tanks, frames
Assembly Checks
Fit, alignment, movement
Electrical And Safety
Cabinet, interlocks, E-stop
Full Run Test
Machine, material, pipe
Factory Acceptance
What you receive
Certificates And Documents
CE, ISO 9001, SGS
Pre-Shipment And Packing
Counted, crated, loaded
FAQ
Witness, records, CE
Inspection Request
Send your acceptance list
Manufacturing Capability
What we machine in house
Settle The Spec, Then Measure The Parts
Many faults that surface at commissioning were decided weeks earlier: a screw cut for a different formulation, a die interface copied from a catalogue, a cabinet part nobody near your plant stocks. That is why our checks begin with what goes into the machine, before anything is bolted together.
Spec Agreed First
Screw type and geometry, diameter and L/D, screw and barrel material and any wear protection are confirmed against the resin or formulation you will really run. For a die head, you approve the drawing before the first cut.
Parts Measured Early
Machined parts are measured before they reach the assembly bench. A part that misses its drawing is made again rather than persuaded into place with a file.
Bore Before Finish
The barrel bore is checked before any surface treatment is applied, so a dimensional error cannot hide under the finish and turn up later as uneven wear.
Known Component Brands
Motors, inverters and electrical parts come from internationally recognised makers, chosen so replacements are easy to buy in your market. Prefer a brand your team already stocks? Name it before the cabinet is finalised.
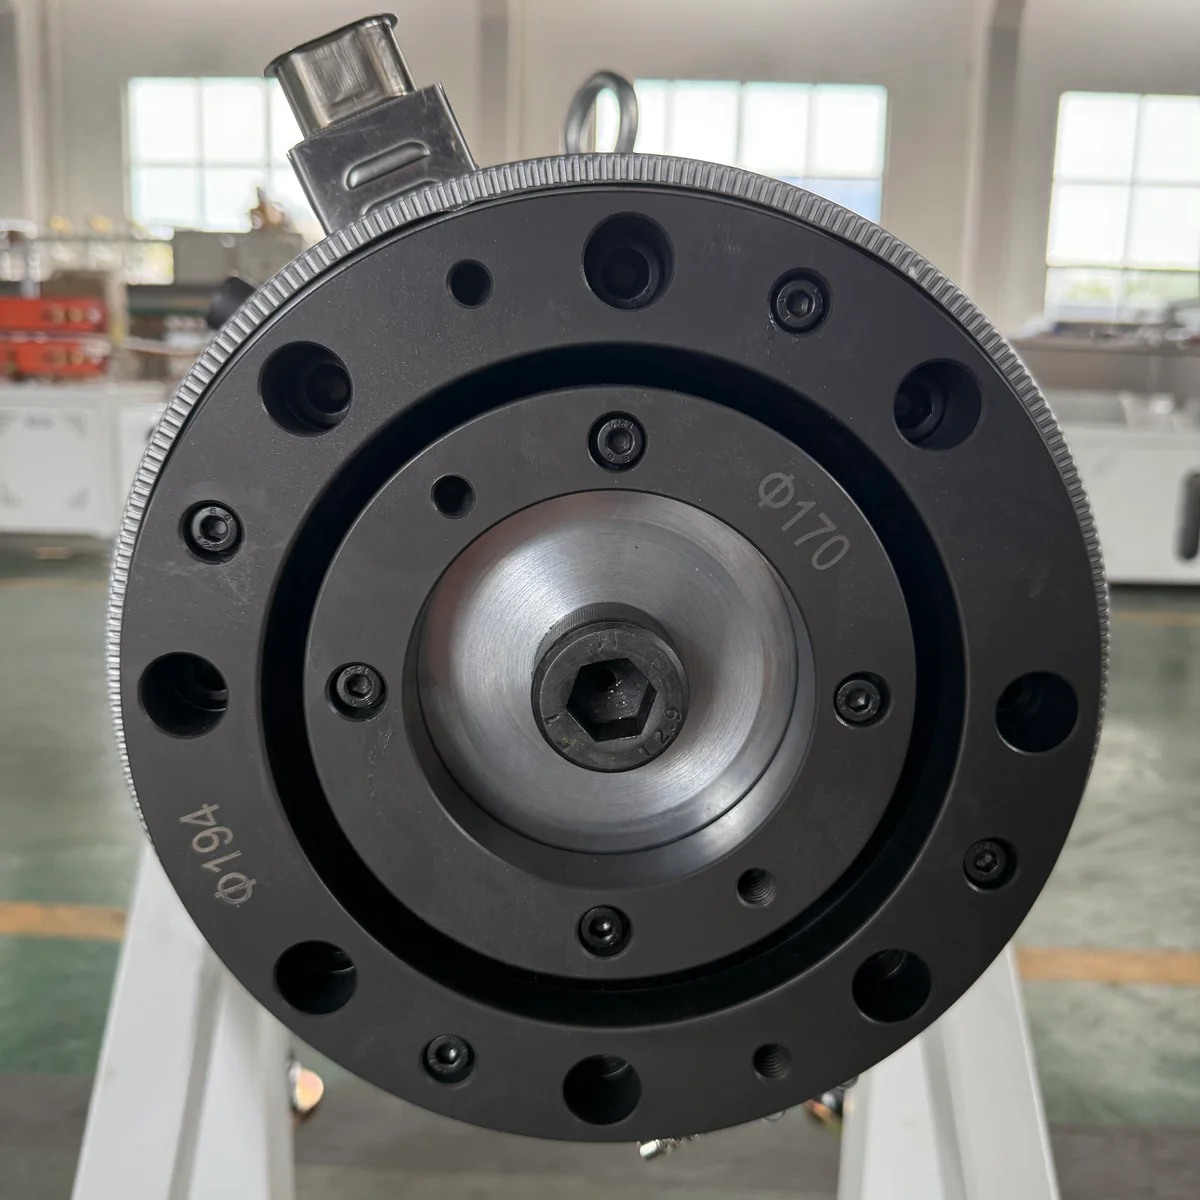
Ordering a replacement head for an extruder you already run? The interface is taken from your machine, not a standard sheet. See how it works on the die head page.
Approved parts are only the start, because the next checks happen while the steel is still being cut, welded and fitted.
Checked Before It Closes Up
Some parts are visible for only a few days of the build. A flow channel ends up sealed inside the die head, spray piping disappears behind tank panels and a base frame vanishes under the machine it carries. These are looked at before they close up.
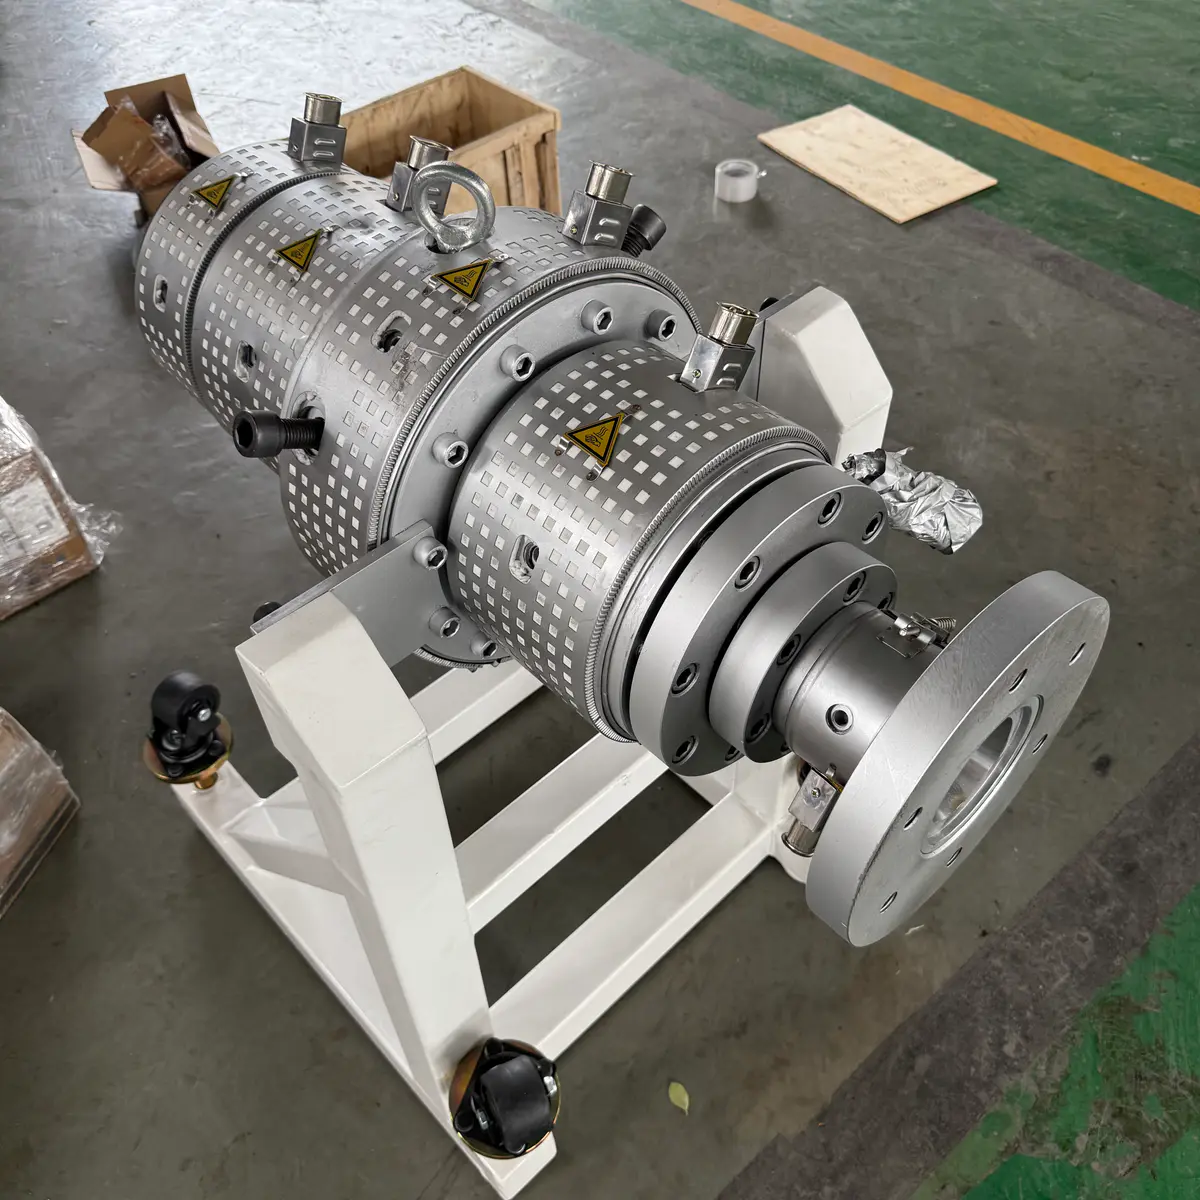
Dimensions As The Work Moves
Critical sizes and mating faces are measured during machining, not only at the end. Flow channels and the die land are ground and polished, then inspected for tool marks where melt could hang up.
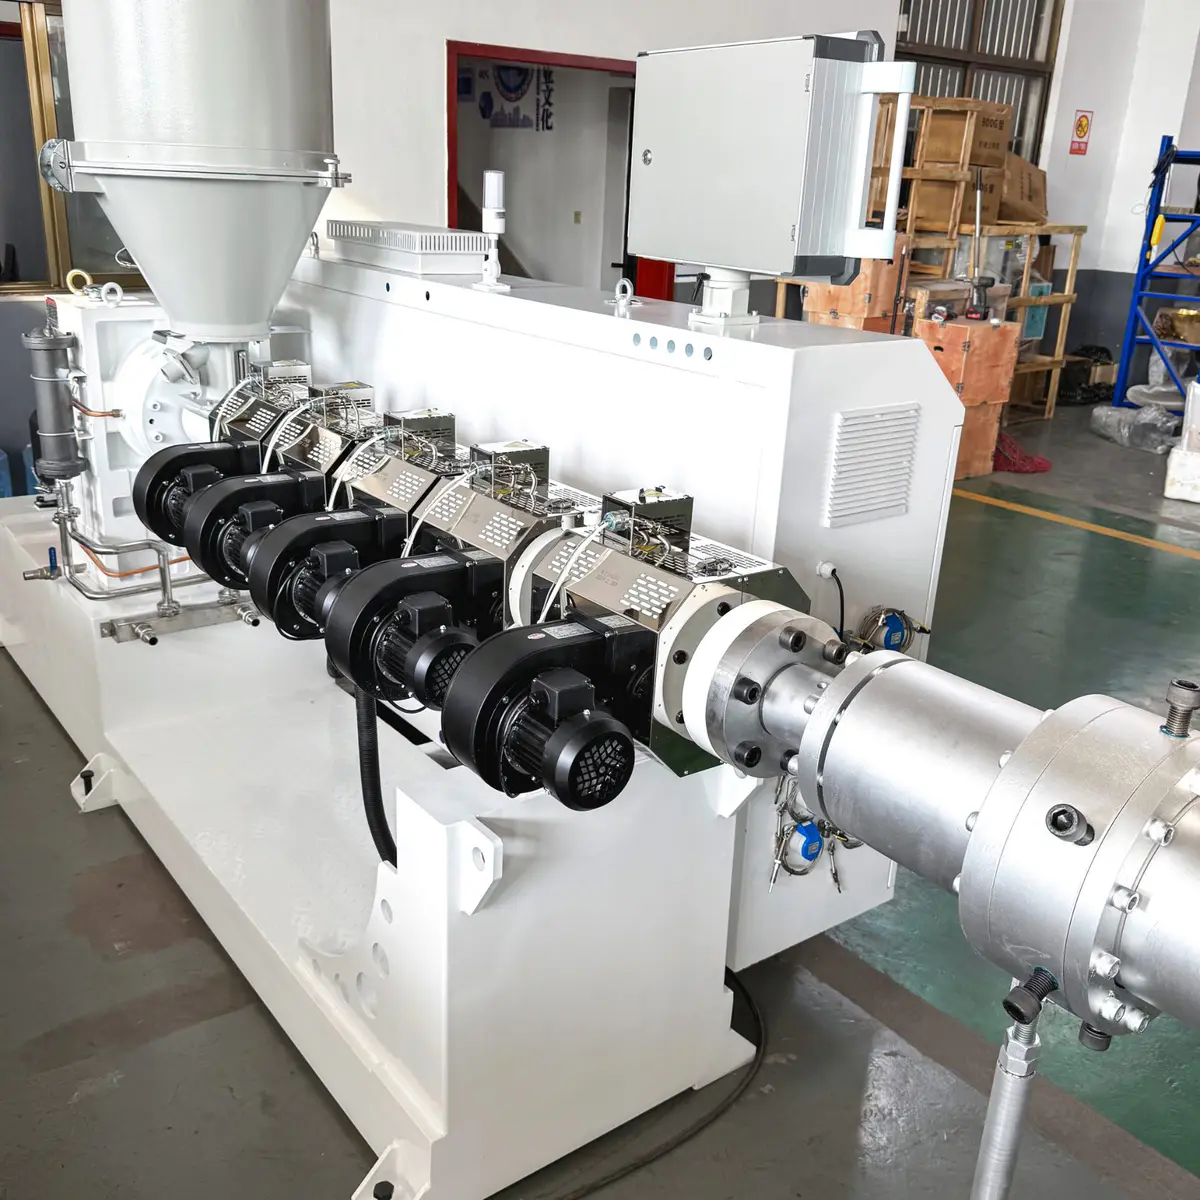
Geometry And Heating Zones
Screw flights are cut to the geometry you approved. Heaters and thermocouples go onto the barrel zone by zone, each one ready to prove itself in the heating test later on.

What Hides Behind The Panels
Weld seams, internal water piping, nozzle layout, vacuum lines and drain points are inspected while the tank is still open. These decide whether cooling stays even a year from now, so ask to see them.
Frames And Bases
Extruder bases are machined flat so the pipe centre height holds once the machine is loaded. On coilers the welded frame is stress relieved and machined flat before the winding station goes on.
Downstream Parts
Belling mandrels and molds, cutter carriages and haul-off caterpillars are built for the pipe range you approved, which is exactly the range they are tested on later.
Build Photos On Request
Want to see your own parts at these stages? We send photos while the work is open, so the first picture you get is not the shipping notice.
Once each part is right, the question becomes whether the parts sit, line up and move together the way the drawing says they should.
Fit, Alignment And Movement, Machine By Machine
A haul-off goes wrong in different ways from a vacuum tank, so assembly checks follow the machine. The common thread is the line: centre height, interfaces and connection points are measured against the layout you approved, so each unit meets its neighbour on your floor.
Extruder
Frame, screw and barrel fit and alignment; centre height and interfaces against the drawing; gearbox torque and lubrication set during the build.
ExtrudersDie Head
Mating faces as the head goes together, component fit, fastening points, and a centring mechanism that really moves the way your operators expect.
Die HeadsVacuum Calibration Tank
Tank travel and positioning, the adjustment points your team will use at installation, centre height and the position of every connection.
Vacuum TanksSpray Cooling Tank
Pipe support rollers, adjustment points and covers through their full range, plus centre height, overall size and water connections.
Cooling TanksHaul-Off
Caterpillar position, parallelism and pipe centreline against your drawing, and on multi-track machines, tracks that run together with no visible speed difference.
Haul-OffsPipe Cutter
Carriage travel, guide movement, positioning and return over the whole stroke, then the clamp action and the mounting of the blade or knife.
CuttersBelling Machine
Mandrel, mold, pipe support and forming position set against the socket drawing, using the tooling that ships with the machine.
BellingWinder
Winding station bearings and shafts, a traverse guide matched to the pipe OD range and tension feedback set for your pipe and coil format.
WindersStacker
Frame, support positions and tilting structure checked under the agreed pipe size and load, with extra care on long or heavy pipe.
StackersEach machine keeps its own inspection plan; anything your order adds goes onto the same sheet.
A machine that fits and moves is ready for power, and the electrical checks are where hidden wiring faults get caught.
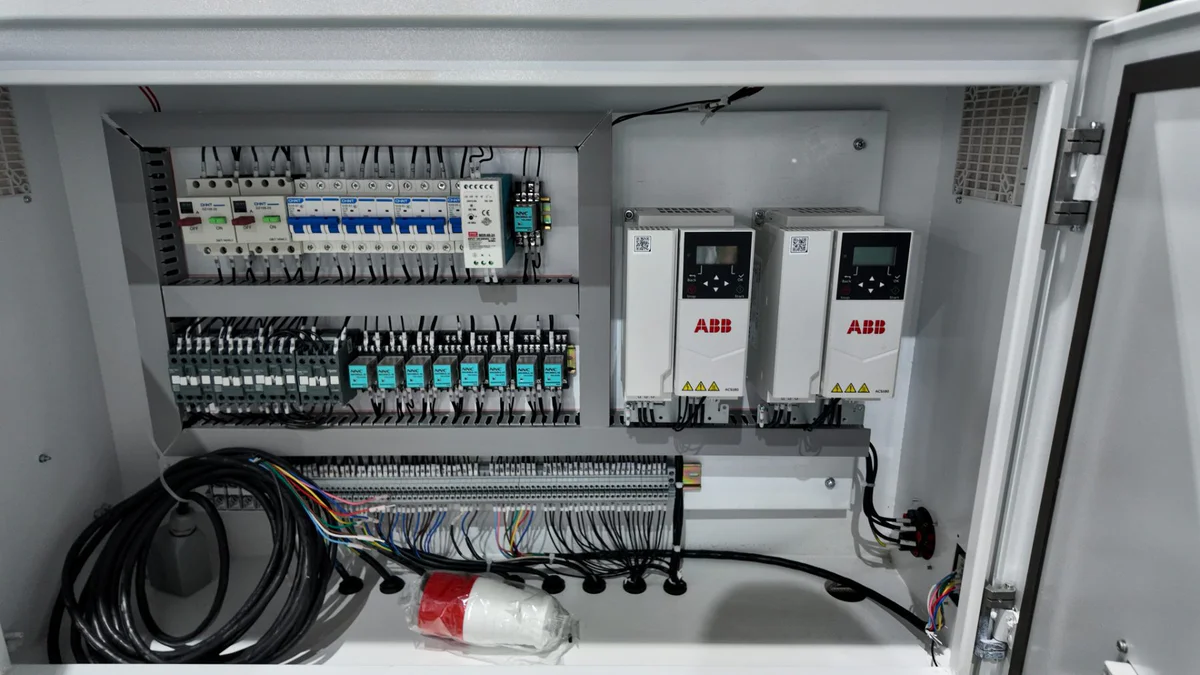

Every Circuit Triggered, Not Just Switched On
Cabinets are built for your supply voltage and frequency and for the safety standard of the market the line goes to. Before a cabinet is closed for shipping, it is worked through the way an operator will use it, one function after another.
Control
- Wiring and terminals against your voltage and standard
- Control buttons and temperature controllers
- PLC program and HMI screens
- Sensors and the signals passed between machines
- Alarm functions, each one triggered
Safety
- Emergency stop circuits
- Interlocks, for example on a discharge valve
- Guards on moving and cutting parts
- Dust or chip extraction on cutters
- Guarding, wiring and marks set for your market
Replacing one machine inside an existing line? Tell us which signals the new unit has to exchange with your equipment and they go onto the test list, because the signal side is where most integration surprises sit.
Powered and safe is still not production, so the run test is where the machine finally meets material and your pipe specification.
Tested Against Your Pipe Spec
Every machine runs in our workshop before it is packed. How far the test goes depends on your scope: a running check proves drive, heat and controls, a material trial proves the process, and a line test puts finished pipe in your hand. The conditions are written down before test day, not argued about after it.
Under Power
Drive, Heat And Controls
- Screw rotation and direction
- Noise and vibration while running
- Main motor and gearbox under drive
- Heating zones reaching and holding setpoint
- Alarms and interlocks responding
- Operating sequence run from the panel
A running check proves the machine turns, heats and stops as it should. It does not prove output, which is why a material trial is worth agreeing wherever your project allows one.
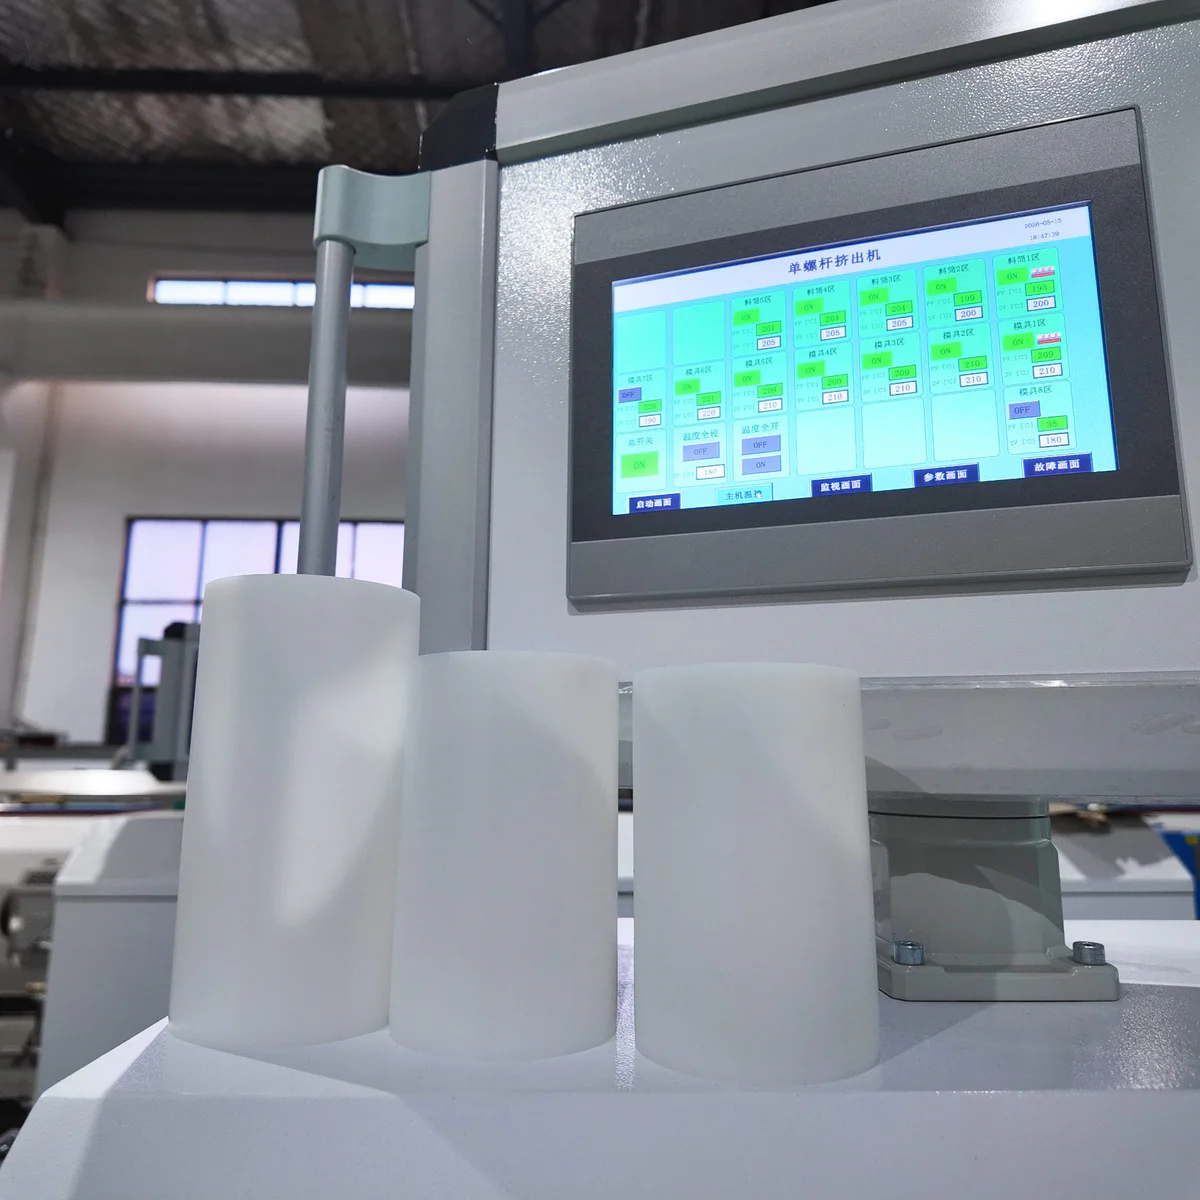
Under Load
Operating Data Recorded
- Actual output in kg/h
- Screw speed
- Motor load
- Barrel temperature by zone
- Melt temperature
- Melt pressure
- How long the rate was held
A material trial runs when testing is part of your scope and suitable material, tooling and downstream equipment are on hand. We say plainly what can and cannot be reproduced in our workshop before you rely on it.
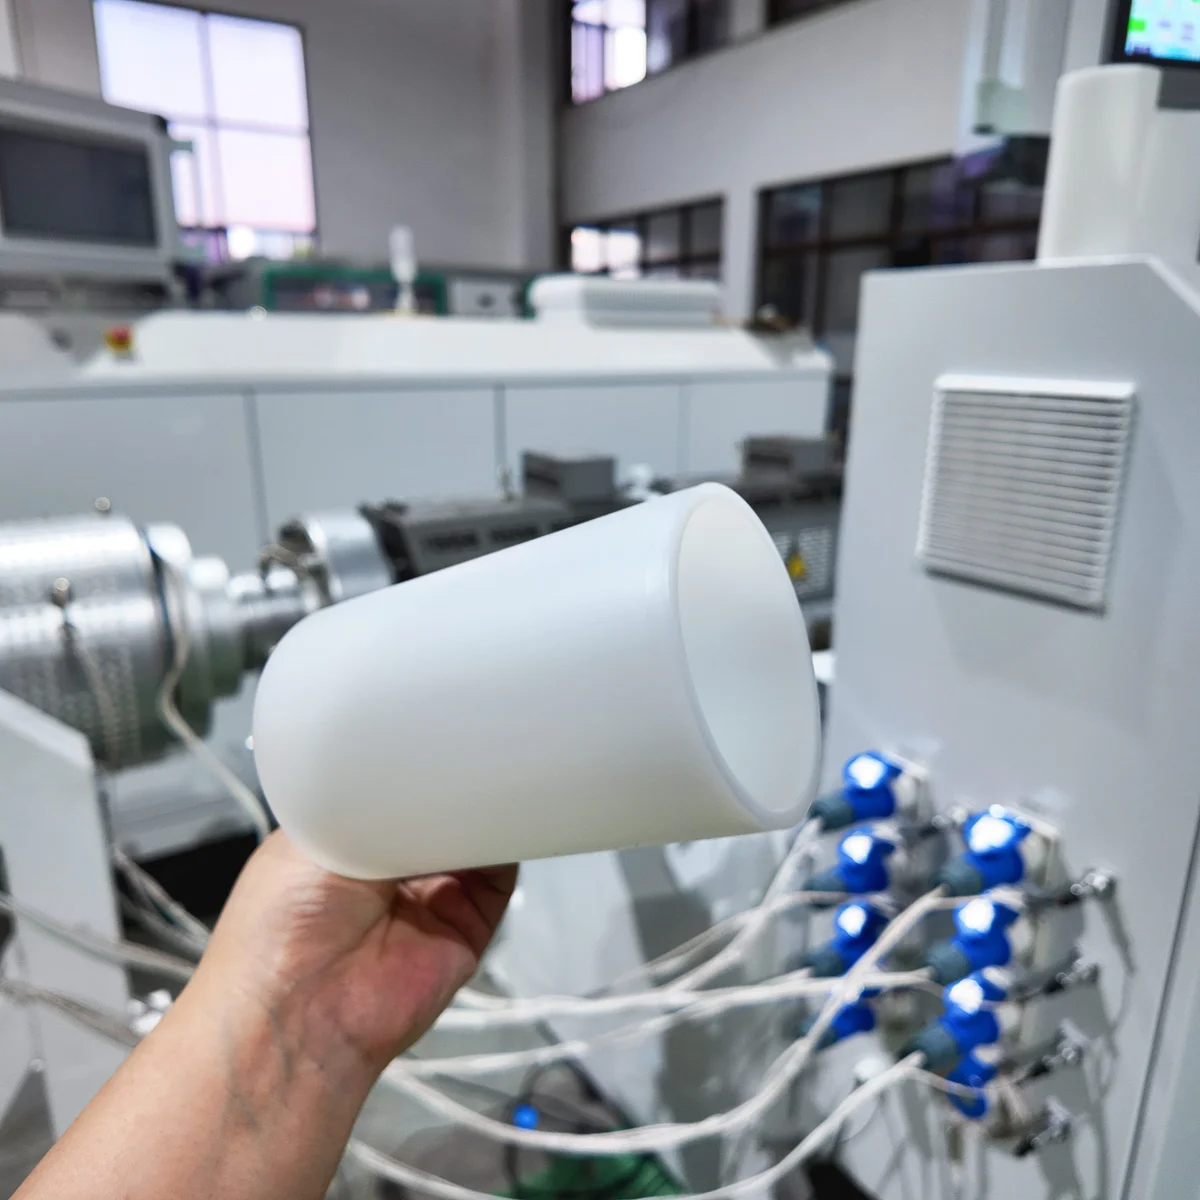
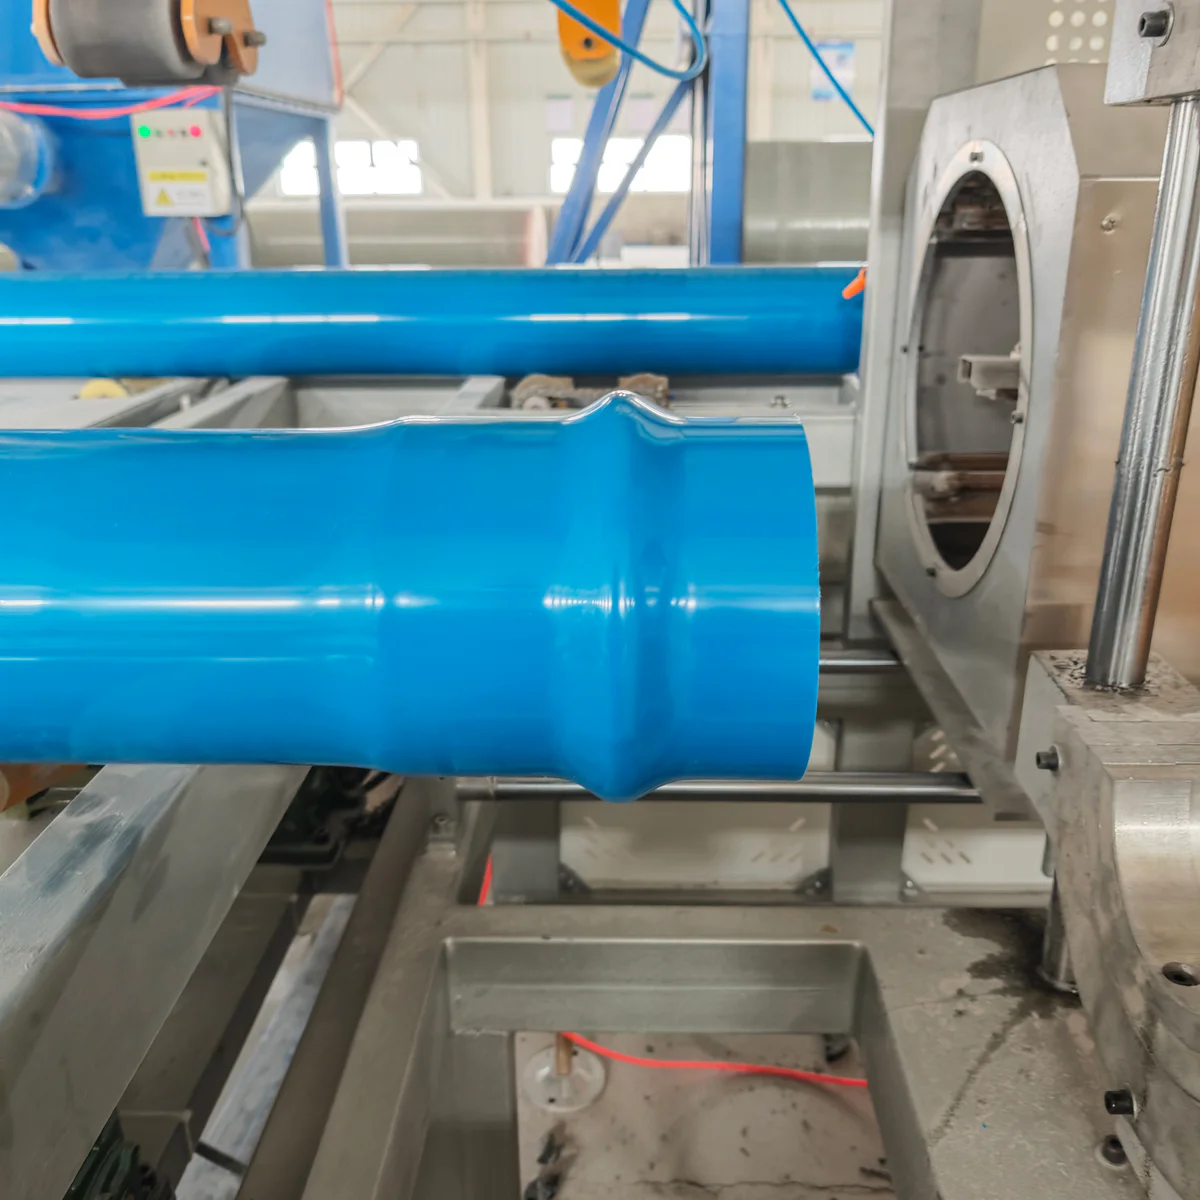
On The Pipe
What The Pipe Is Judged On
- Outside diameter holding steady
- Wall thickness at agreed points
- Ovality
- Inner and outer surface
- Colour stripe in position
- Cut length and a clean end
- Socket shape on belled pipe
- Coil quality on small pipe
Put the targets in writing with your test request: material and pipe size, target output, surface standard, wall measuring points and the tolerance you work to, the melt window, and how long the run has to hold.
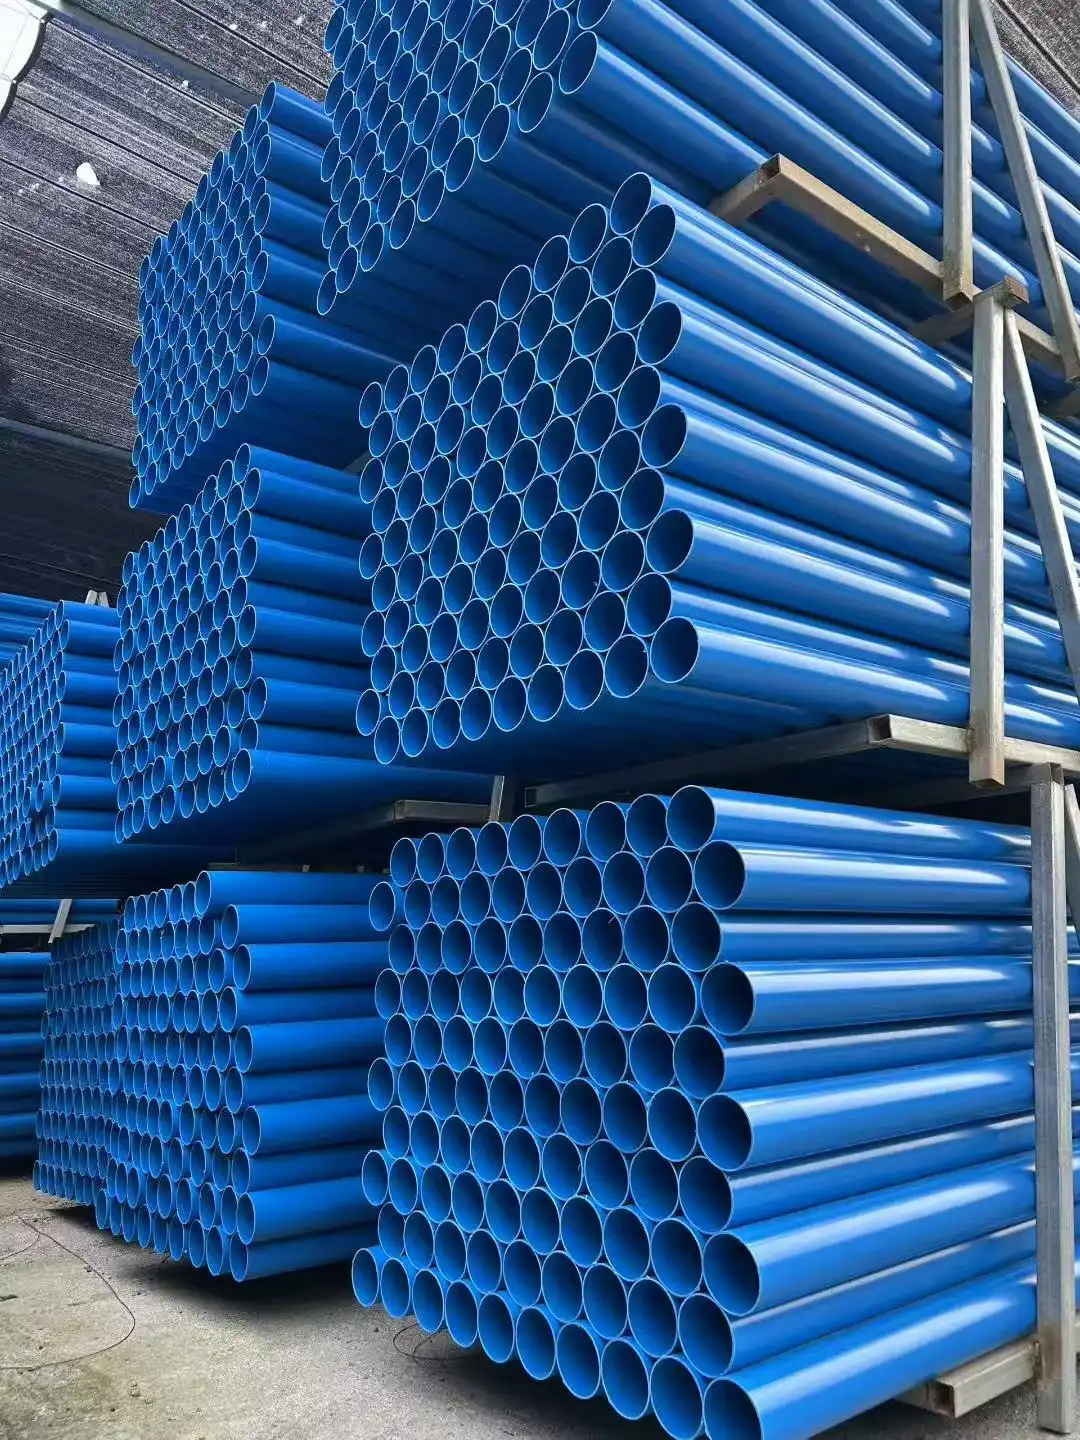
After The Die
Proof From The Downstream Machines
- Cut length and squareness
- End face free of heavy burrs
- Chamfer angle and depth
- Socket dimensions and roundness
- Joint fit with the gasket, where used
- Coil ID, OD and width
- Several cycles in a row
One good piece proves very little. Downstream checks run across consecutive pipes, sockets or coils, so you see the same result repeat instead of a single lucky sample.
Planning a complete line rather than one machine? Start from the pipe extrusion lines overview, then agree the test with Maggie.
A test only counts when both sides agreed the pass list beforehand and the result reaches you in a form you can keep.
What You Receive Before The Crate Is Closed
Factory acceptance is agreed with you rather than announced to you. The scope is set against your machine configuration and the test conditions your project allows, and anything you want added is reviewed before manufacturing starts.
Before Manufacturing
Send your own acceptance items with the order. We confirm which of them can be tested here and put the agreed list in writing, so test day holds no surprises for either side.
On Test Day
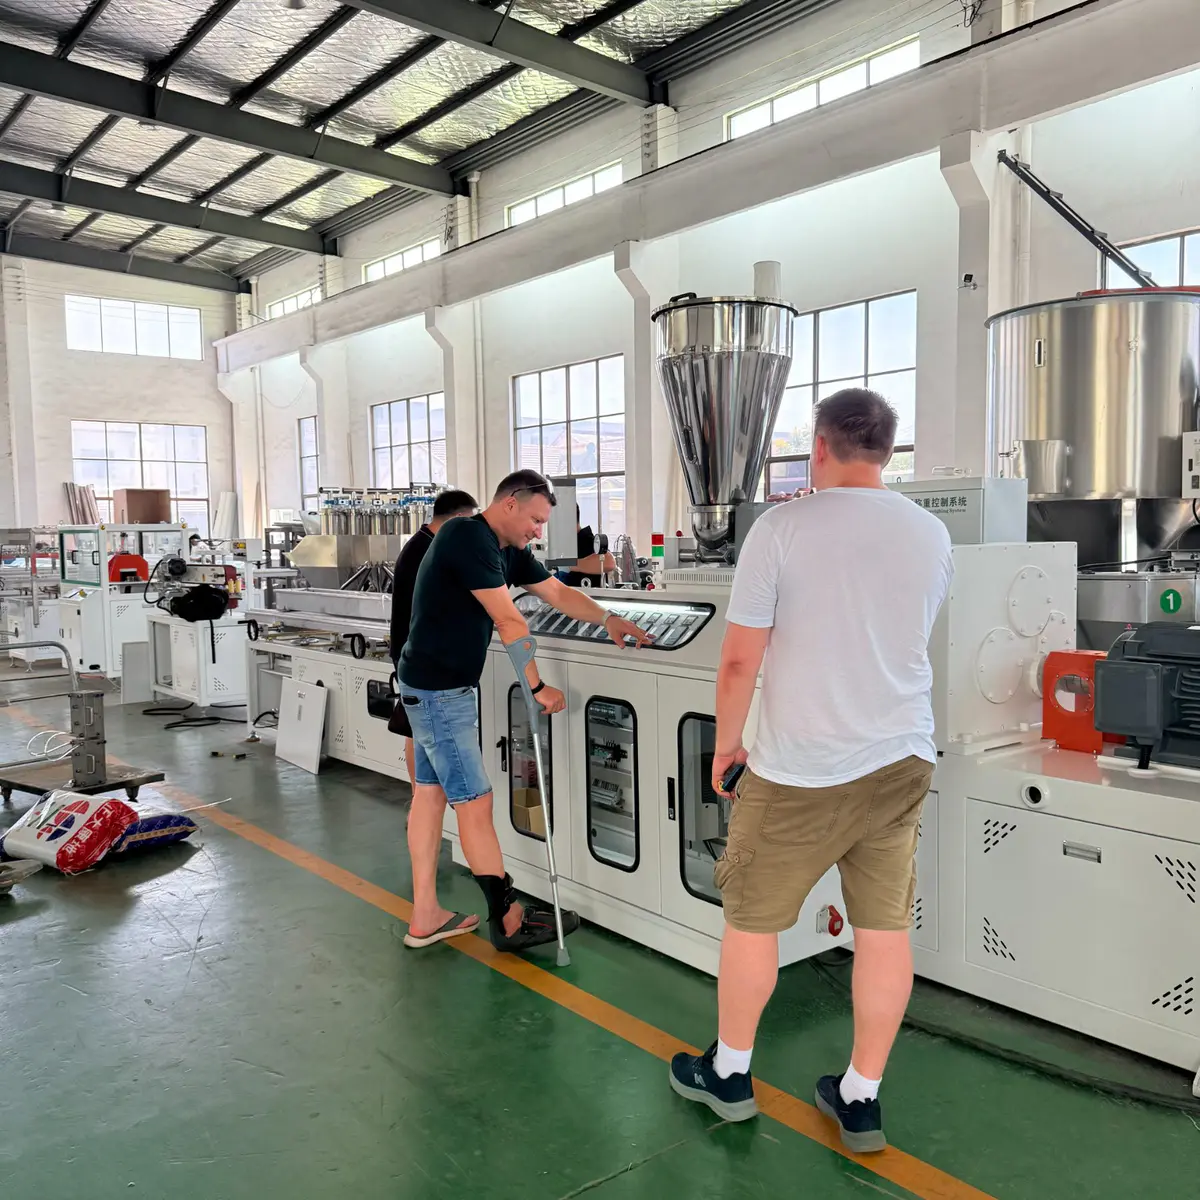
Attend in person, join a video call with your engineer, or send a third-party inspector. Tell us early and the test is booked around your visit.
Before Packing
The record, photos and video reach you while the machine is still in our workshop. Anything that needs adjusting is put right on our floor, where it costs a day instead of a container and a service trip.
Six Things Your Acceptance Can Include
Inspection Report
The agreed items and the result recorded against each one.
Run Test Video
Your own machine or line running, not a stock clip.
Photo Set
Close views of the build and the test stages you asked about.
Sample Pipe
Pipe from the trial, prepared when your scope includes a material run.
Measured Results
Dimensions, operating data and the test sheet for the items agreed.
Inspection Points
The checkpoints you named, shown one by one and kept as a signed record.
The test record is one piece of paper; the certificates and manuals that travel with the machine matter just as much at customs and on site.

CE, ISO 9001 And SGS, Plus The Papers Your Team Needs
A line bound for Europe needs CE paperwork that is genuine and matches the machine on the truck. Our CE verification of conformity names Zhangjiagang Qinxiang Machinery Co., Ltd. as both applicant and manufacturer, and the certificate and technical file are supplied with your order. Guarding, wiring and marking are set for the market the line ships to.
Documents That Ship With The Order
- Operation manual for your configuration
- Electrical and wiring diagrams
- Layout drawings and installation guidance
- Inspection report and test record
- Packing list and export documents
- Recommended spare parts list
- Final die drawings and tooling identification
- CE certificate and technical file
With the paperwork in order, the final check happens around the crate itself, just before the container door shuts.
Counted, Marked And Crated Before Loading
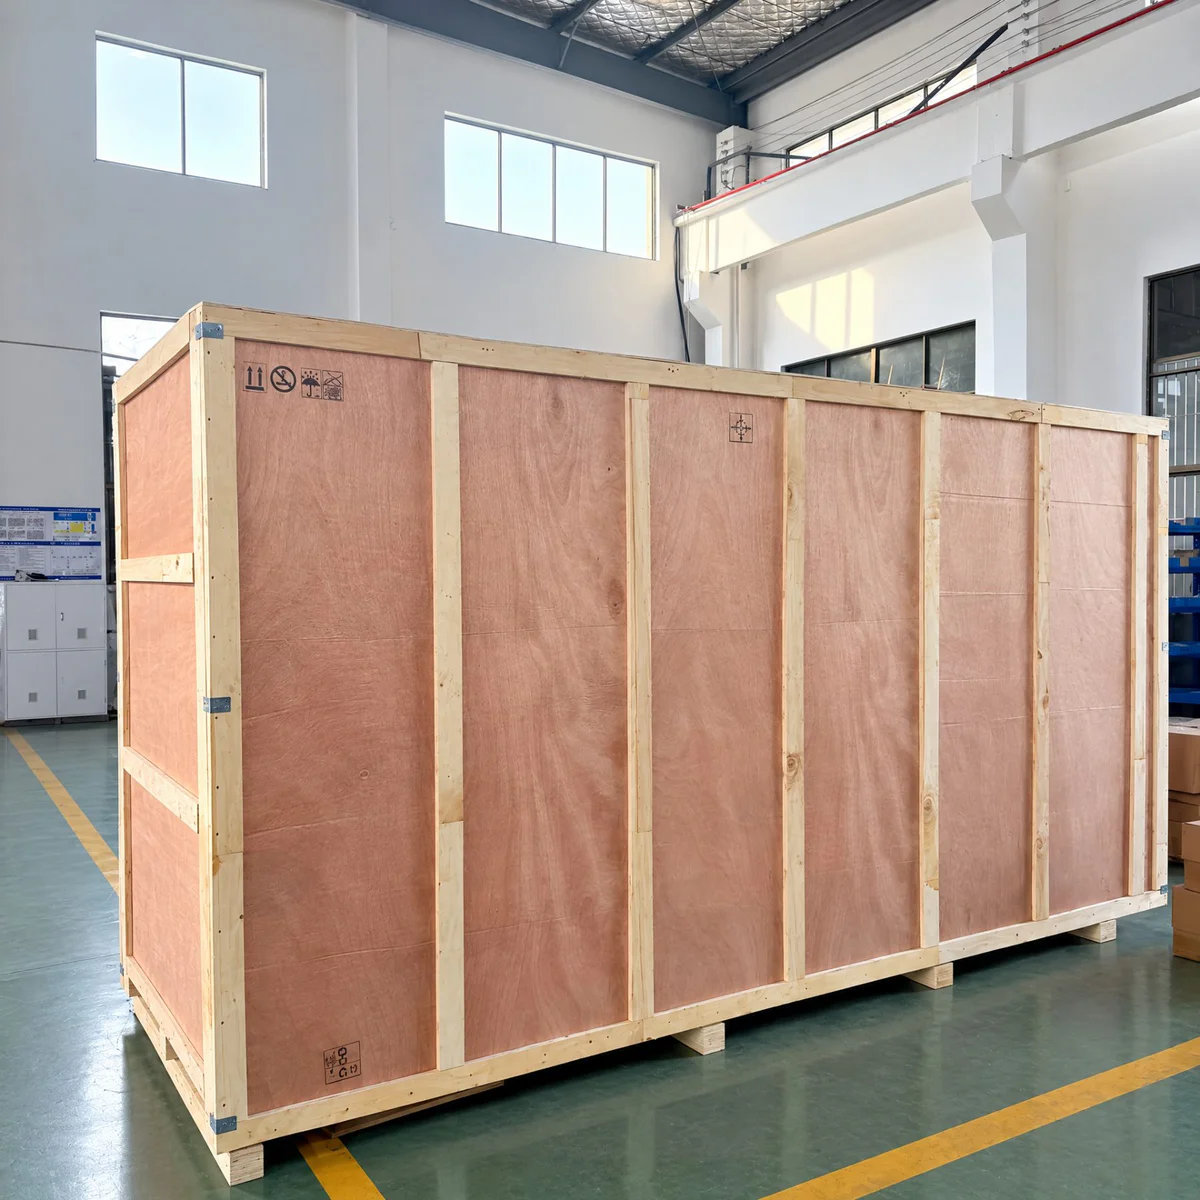
A missing mandrel or manual can stall a start-up as surely as a fault. Before loading, the shipment is checked as a whole: machines, parts, documents and the crates that carry them.
Parts And Spares
Machine parts and the spare parts on your order are checked off against the packing list.
Tooling Sets
Every die, mandrel, sleeve and adapter you ordered is counted, since one missing piece can hold up commissioning.
Documents In The Crate
Manual, electrical diagram and export papers are confirmed before the lid goes on.
Marks And Packing
Shipping marks and the packing itself are inspected before the container is loaded.
Loading Photos
You receive loading photos together with the packing list and shipment documents.
Which spare parts are worth adding to the crate depends on how your machine is built. See how that list is put together on Manufacturing Capability.
Quality Control Questions
What buyers usually ask before they agree an inspection plan. Anything else, ask Maggie directly.
Yes. Every machine runs in our workshop before packing, at minimum as a running check of drive, heating, controls and alarms. A material trial or a full line test is added when your scope includes it and suitable material and equipment are available.
Yes. Attend in person, join a video call with your engineer, or send a third-party inspector in your place. Let us know early so the test date can be set around your visit.
Send them before manufacturing starts. We review each item, confirm which can be tested in our workshop and put the agreed list in writing, so the final check is measured against that list and nothing else.
The inspection record for the agreed items, photos of the build and test, and a video of your machine running. When a material trial is part of the scope, you also get the recorded operating data and the results measured on the sample pipe.
It is put right in our workshop before packing. A machined part that misses its drawing is made again rather than adjusted at the bench, and the item is checked again before the record goes to you.
Our CE verification of conformity covers our extruders and names Zhangjiagang Qinxiang Machinery Co., Ltd. as applicant and manufacturer. Lines for the EU are built and documented to CE requirements, the certificate and technical file come with your order, and Maggie can send you a copy before you buy.
Yes. Motors, cabinets and safety devices are built for your supply voltage and frequency and the standard of your market, and the electrical tests are carried out in that configuration.
Where it fits the scope, yes. Tell us early and send material or pipe samples in good time; we confirm beforehand whether your pipe size, tooling and downstream setup can be reproduced in our workshop.
Agree Your Inspection With Maggie
Tell us the machine or line, your pipe specification and anything you want tested or certified. Maggie replies within 24 hours with a proposed inspection scope and a quote.
Maggie
Sales, QTech Machinery
Replies within 24 hoursI read every request from this page myself. Send the pipe you need to make and the checks that matter to you, and I come back with the test scope, the documents you will receive and a quote.
If something on your list cannot be reproduced in our workshop, I will tell you before you order, not on test day.
Maggie
Sales, Zhangjiagang Qinxiang Machinery Co., Ltd.
- Inspection scope agreed before manufacturing
- Test record, photos and video before packing
- Witness in person, by video or through an inspector
- CE verification of conformity on request
Tell Us What Has To Be Proven
Fields marked are required.