WhatsApp Maggie
Project Case · Asia-Pacific

PE Core Pipe Extrusion Line for Roll Core Tube Manufacturing

WhatsApp Maggie
PE Core Pipe Extrusion Line for Roll Core Tube Manufacturing

Project Type

Complete Extrusion Line

Machines

Dosing & Feeding Equipment, Extruder, Haul-Off Machine, Pipe Extrusion Die Head, Vacuum Calibration Tank

Material

PE/HDPE

Application

Agricultural Irrigation, Cable Protection, Drainage & Sewage, Gas Distribution, Industrial Pipes, Water Supply

Region

Asia-Pacific, Europe, Latin America, Middle East and Africa, North America

01

Project Overview

QTech-Machinery completed a customized PE core pipe extrusion line project for a customer producing industrial roll core tubes. The customer required a production system for manufacturing PE core tubes used in film rolls, electronic material winding, packaging rolls, foil rolls and other industrial roll-support applications.

Different from general water pipe production, this project focused on PE roll core pipe manufacturing, where pipe roundness, wall thickness stability, cutting accuracy and end-face quality are important for downstream winding performance. The complete production line was designed to cover material melting, pipe forming, vacuum sizing, cooling, traction, length measuring and automatic cutting.

The supplied solution included an SJ75/33 single screw extruder, PE core pipe mould, 160 vacuum calibration tank, three-claw haul-off unit and 160 chipless cutting machine. With coordinated line height, PLC operation and servo traction control, the system helped the customer establish a practical and reliable PE winding core pipe production line for continuous operation.

02

What The Customer Needed

The customer needed a complete PE core tube extrusion equipment solution that could produce strong and dimensionally stable PE roll core pipes. The final products would be used as winding cores, so the pipe had to keep good roundness, sufficient rigidity, accurate length and smooth cutting edges.

Main project requirements included:
1. Complete PE core pipe production from extrusion to cutting
2. Stable PE material melting and continuous extrusion output
3. Mould design suitable for PE roll core tube forming
4. Support for pipe inner diameter around 77 mm
5. Capability for multiple wall thickness options
6. Reliable vacuum calibration for roundness control
7. Efficient spray cooling to stabilize pipe shape
8. Strong haul-off force for thick-wall PE core tubes
9. Servo-driven traction for speed synchronization
10. Encoder-based pipe length measuring
11. Chipless cutting to reduce dust and pipe-end burrs
12. Touch screen control for easy parameter setting
13. Industrial electrical configuration for long-term use
14. Straight-line equipment layout with unified center height
The customer expected the line to be simple to operate, durable, and suitable for daily production of PE core pipes in different wall thicknesses.

03

What We Supplied

QTech-Machinery supplied a complete PE core pipe extrusion line according to the customer’s product size, production process and factory layout. The line was engineered as a continuous extrusion system for PE roll core tube production, combining stable output with accurate downstream control.

The main extrusion section used an SJ75/33 single screw extruder with alloy screw and barrel, inverter speed control, segmented heating and PLC-based operation. This ensured stable PE plasticizing and continuous material flow into the mould.

The forming section used a customized PE core pipe mould designed for the required inner diameter and wall thickness range. After mould forming, the pipe entered the 160 vacuum calibration tank, where vacuum sizing and spray cooling helped maintain pipe roundness and surface quality.

For downstream pulling, QTech-Machinery configured a three-claw haul-off machine with servo motors. This allowed accurate speed matching between extrusion output and pipe traction. At the end of the line, the 160 chipless cutting machine completed automatic cutting according to encoder-measured length, helping produce clean pipe ends for roll core applications.

The complete system was delivered as an integrated PE winding core pipe machine, suitable for stable and repeatable production.
Key Configuration

Machines And Settings In This Project

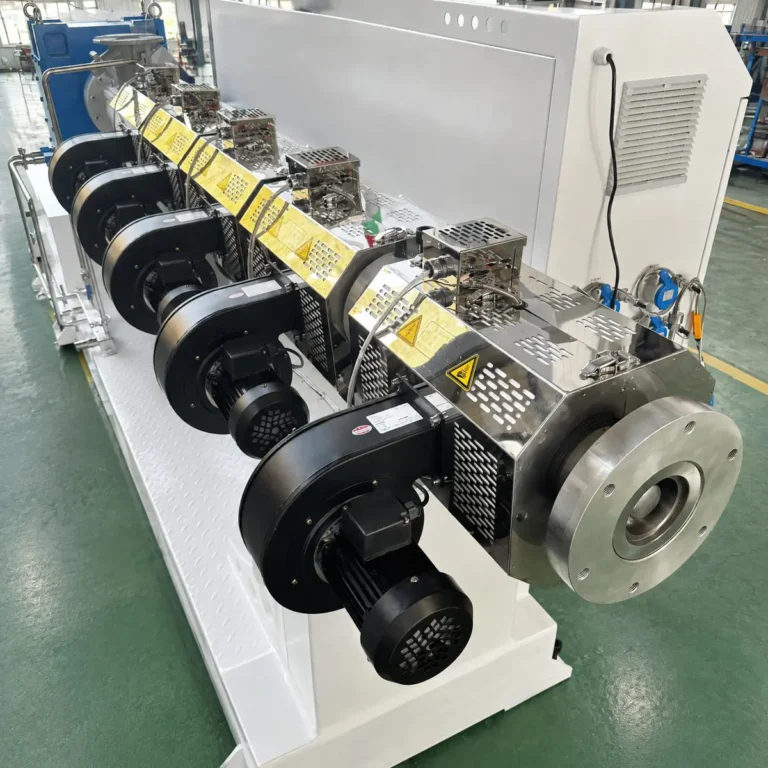
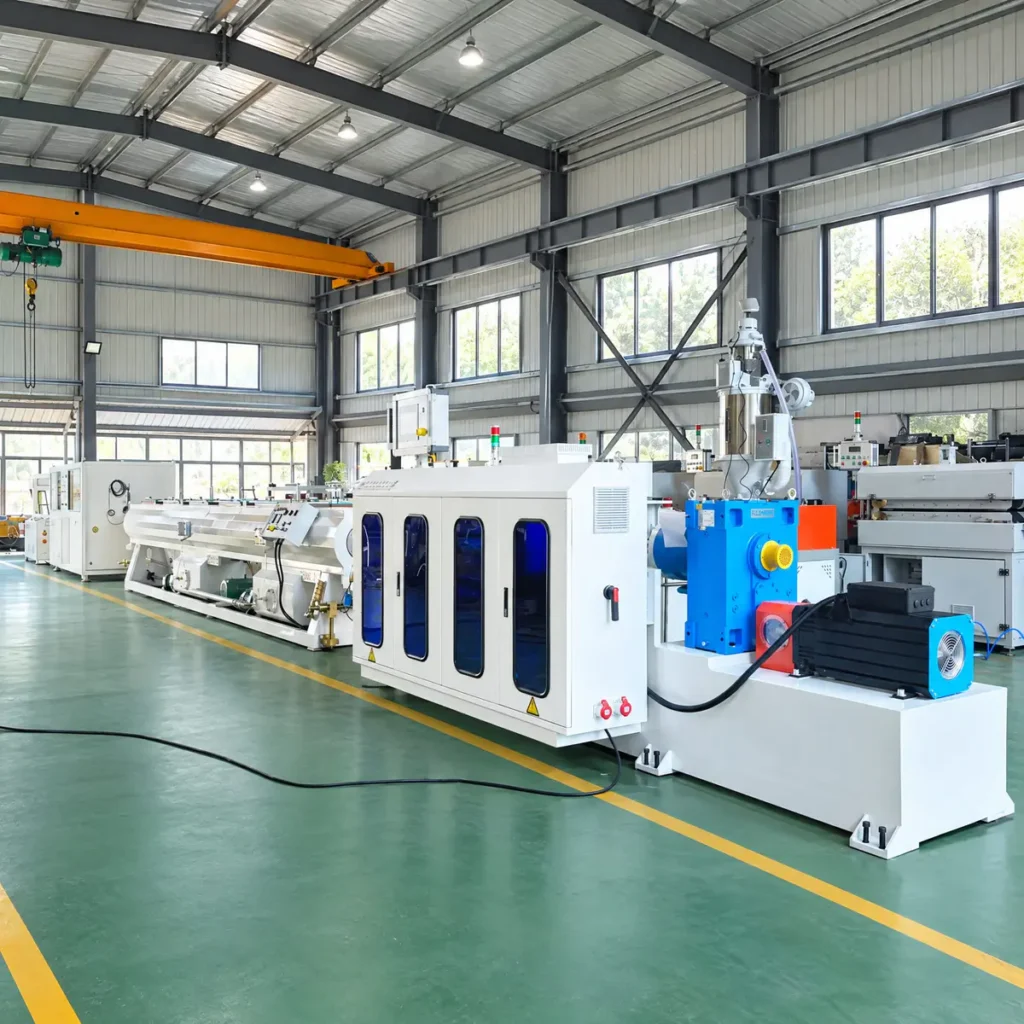
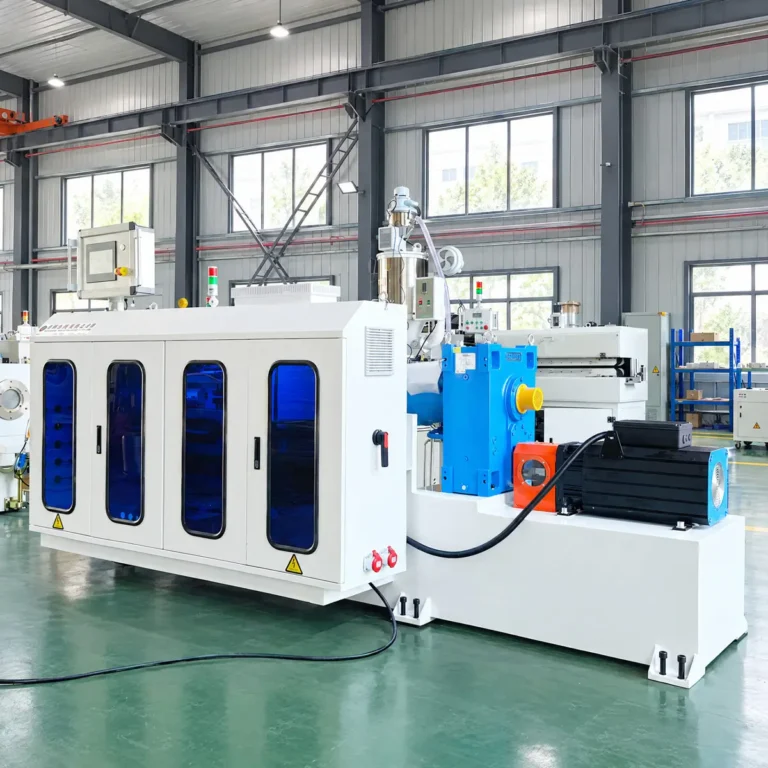
Plastic extrusion machine with control cabinet and extruder body installed on a green floor in a modern factory workshop

SJ75/33 Single Screw Extruder

1. Extruder model: SJ75/33 single screw extruder selected for PE core pipe and PE roll core tube production.
2. Screw specification: 75 mm screw diameter provides suitable output capacity for medium-size PE core tubes.
3. L/D ratio: 33:1 screw length-to-diameter ratio supports sufficient plasticizing time and melt uniformity.
4. Screw material: 38CrMoAlA alloy steel screw with heat treatment and nitriding for improved wear resistance.
5. Barrel material: Nitrided 38CrMoAlA barrel offers strong hardness and long working life under continuous extrusion.
6. Main drive power: 45 kW motor supplies stable torque for PE material processing.
7. Speed adjustment: Inverter-controlled screw speed allows flexible output adjustment during production.
8. Heating system: Cast aluminum heating zones help maintain stable barrel temperature during melting.
9. Cooling design: Barrel cooling fans assist temperature balance and prevent overheating in each section.
10. Operation control: Siemens PLC, Siemens HMI, pressure sensor, Schneider contactors and Chint electrical parts support convenient monitoring and operation.

Closeup view of a plastic extrusion machine screw and barrel with multiple barrel heaters and cooling fans installed

PE Core Pipe Mould System

1. Mould application: Customized for PE core pipe, PE roll core tube and PE winding core pipe extrusion.
2. Product specification: Designed for pipe inner diameter around 77 mm according to the customer’s roll core requirement.
3. Wall thickness range: Supports different wall thicknesses such as 6 mm, 7 mm, 8 mm, 9 mm and 10 mm through suitable tooling and process settings.
4. Melt distribution: Internal flow channel design helps distribute molten PE evenly before pipe shaping.
5. Pipe wall control: Mould structure supports stable wall thickness and reduces uneven pipe eccentricity.
6. Surface forming: Smooth forming surfaces help improve outer and inner pipe appearance.
7. Heating interface: Equipped with mould heating and temperature sensing connections for process control.
8. Installation compatibility: Designed to match the SJ75/33 extruder and downstream vacuum calibration section.
9. Adjustment convenience: Allows commissioning adjustment to fine-tune pipe wall and forming condition.
10. Production purpose: Suitable for manufacturing PE core tubes used in film winding, foil winding and industrial roll packaging.

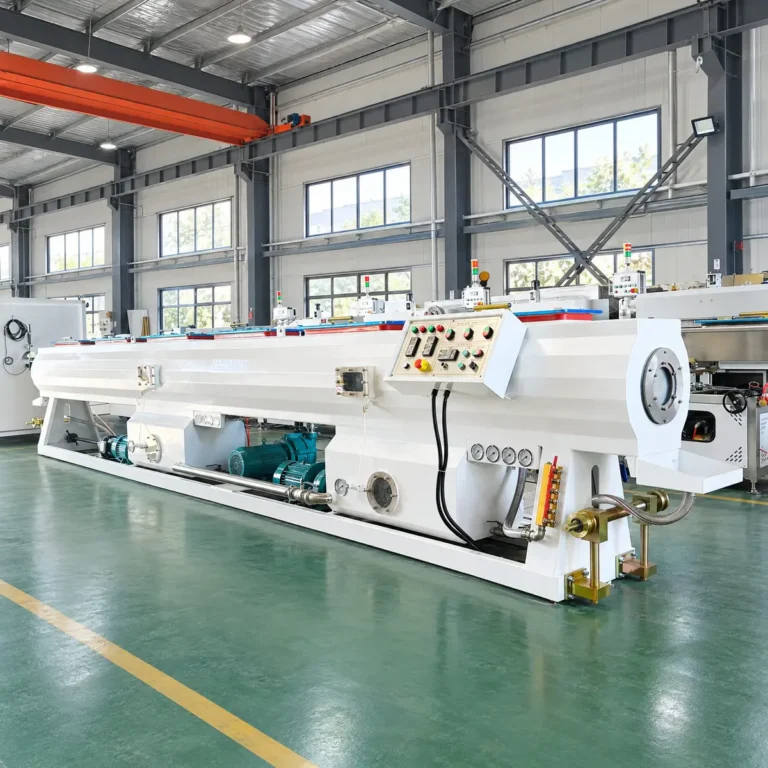
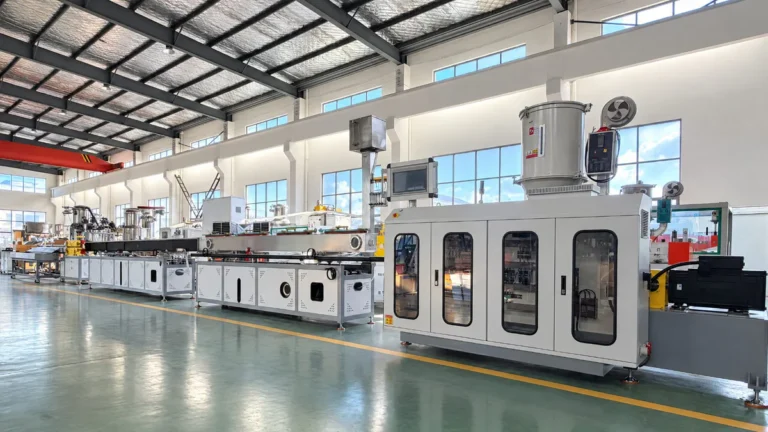
White vacuum calibration tank with control panel situated in a spacious factory workshop with windows and overhead crane

160 Vacuum Calibration Tank

1. Tank model: 160 vacuum calibration tank suitable for PE core pipe extrusion lines.
2. Tank length: 9-meter tank body provides enough distance for vacuum sizing and cooling.
3. Applicable range: Designed for pipe sizing within the matching 160 mm pipe production range.
4. Vacuum control: Adjustable vacuum range of 0.02–0.08 MPa helps control pipe roundness and outer diameter.
5. Tank material: SUS304 stainless steel body improves corrosion resistance and service life.
6. Plate thickness: 3 mm stainless steel structure provides strength for long-term industrial operation.
7. Vacuum pump: 5.5 kW vacuum pump supplies stable negative pressure for calibration.
8. Cooling system: Water pump and spray cooling system help remove heat quickly from the formed PE pipe.
9. Position adjustment: Tank can be adjusted forward/backward, left/right and up/down for line center alignment.
10. Auxiliary control: Water level control, water temperature display, vacuum regulating valve and vacuum alarm support safer operation.

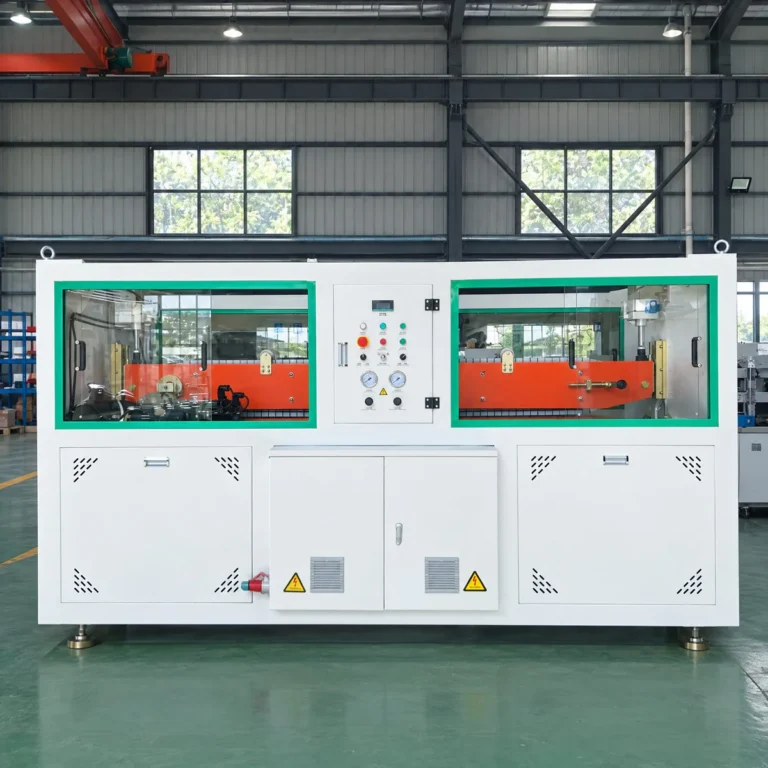
White enclosed auxiliary extrusion machine with control panel and gauges, positioned in a spacious industrial workshop

Three-Claw Haul-Off Machine

1. Haul-off type: Three-claw structure provides stable clamping around the PE core pipe.
2. Machine length: Approximate total length of 2800 mm supports stable downstream traction.
3. Effective contact length: Around 2000 mm effective hauling length increases pipe holding stability.
4. Speed range: Pulling speed adjustable from 0.2 to 3 m/min for different wall thicknesses and output settings.
5. Drive configuration: Three 1.5 kW servo motors provide precise and synchronized traction control.
6. Reducer system: K-series reducers ensure reliable torque transfer and steady mechanical running.
7. Traction capacity: Maximum pulling force of about 1200 N supports thick-wall PE core pipe production.
8. Clamping method: Pneumatic pressing control allows adjustable pipe holding force.
9. Speed synchronization: Servo control helps match haul-off speed with extruder output to maintain pipe size consistency.
10. Measuring function: Encoder meter-counting system records pipe length and sends signals for automatic cutting.

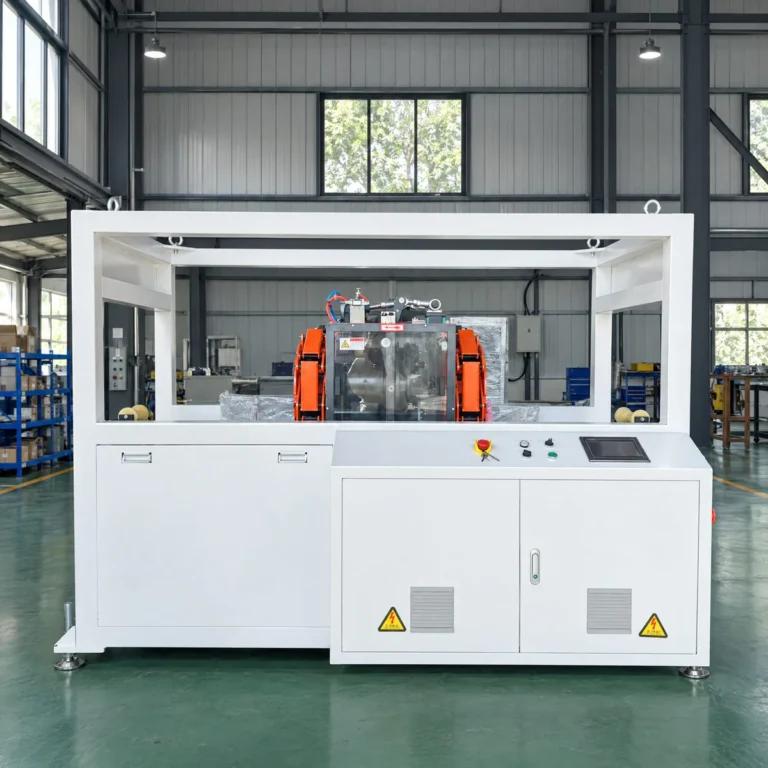
White industrial cutting machine with orange components positioned in a factory workshop

160 Chipless Cutting Machine

1. Cutting model: 160 chipless cutting machine configured for PE roll core tube production.
2. Cutting range: Suitable for pipe diameters from 50 mm to 160 mm.
3. Cutting method: Rotary chipless cutting reduces cutting dust and plastic chips.
4. Blade feeding: Pneumatic blade feeding provides stable cutting action during automatic operation.
5. Pipe support: Clamping and support structure keeps pipe stable during cutting.
6. Length control: Cutting is triggered by encoder measurement according to the preset pipe length.
7. Cutting accuracy: Automatic fixed-length cutting helps improve product consistency.
8. End-face quality: Designed to produce smoother pipe ends suitable for winding core applications.
9. Operation integration: Works with the haul-off machine and PLC control system for continuous line operation.
10. Application advantage: Suitable for PE core tubes where clean cutting and reduced debris are important for packaging and roll handling.

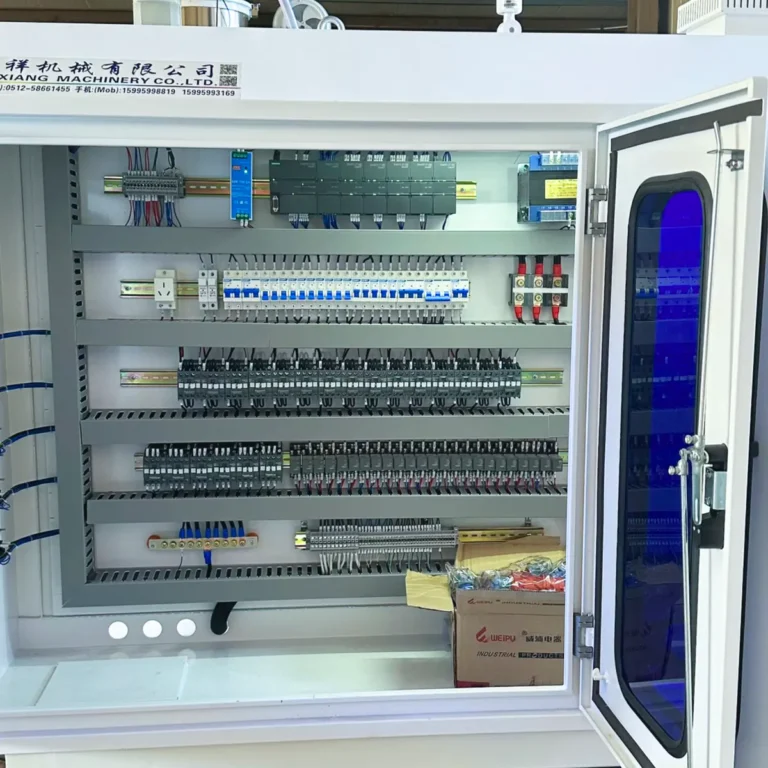
Open electrical control cabinet with organized wiring, circuit breakers, terminal blocks, and a box of connectors

Electrical and Control System

1. Control platform: Siemens PLC controls key production actions and line coordination.
2. Human-machine interface: Siemens touch screen allows operators to set parameters and monitor running status.
3. Main electrical components: Schneider contactors are used for reliable switching and control.
4. Auxiliary electrical parts: Chint electrical components support stable operation and convenient maintenance.
5. Pressure monitoring: Melt pressure sensing helps operators observe extrusion condition.
6. Speed control: Extruder and haul-off speeds can be adjusted to match production requirements.
7. Temperature management: Barrel and mould temperature settings can be controlled by zones.
8. Alarm function: Vacuum alarm and basic operation alarms help reduce production risks.
9. Line integration: Electrical system connects extrusion, calibration, hauling and cutting into one coordinated production line.
10. Operator convenience: Touch screen operation reduces manual adjustment complexity and improves daily production efficiency.

Project Photos

From Testing To Shipment

Project Videos

Watch This Line Running

PE Core Pipe Extrusion Line for Roll Core Tube Manufacturing

PE Core Pipe Extrusion Line for Roll Core Tube Manufacturing

Project Result

How The Line Performs

After installation and commissioning, the PE core pipe extrusion line supplied by QTech-Machinery achieved stable continuous operation. The customer was able to produce PE roll core tubes with consistent pipe shape, smooth surface and reliable fixed-length cutting.

The extrusion section provided steady PE plasticizing and output, while the customized mould helped form the required core tube size. The vacuum calibration tank improved pipe roundness and dimensional stability, and the spray cooling system supported faster shape setting after extrusion.

The three-claw servo haul-off machine maintained stable pipe traction, reducing speed fluctuation during production. The encoder measuring system and chipless cutting unit helped the customer obtain accurate pipe lengths and cleaner pipe ends, which are important for roll core products used in winding and packaging industries.

Through this project, QTech-Machinery helped the customer build a practical PE roll core tube production line with:
1. Stable extrusion output
2. Good pipe roundness
3. Adjustable wall thickness production
4. Smooth pipe surface quality
5. Reliable hauling performance
6. Accurate length measuring
7. Cleaner chipless cutting
8. Easy touch screen operation
9. Integrated line control
10. Suitability for long-term industrial production
This project demonstrates QTech-Machinery’s capability to provide customized PE core tube extrusion equipment for customers in film packaging, electronic material winding, foil roll, industrial material roll and plastic core pipe manufacturing sectors.

Related Cases

More Projects Like This

All Cases
Configuration Request

Get A Line Configured Like This One

Tell us your pipe range and material. Maggie replies with the machine list, the layout, and a price based on this project.

  • Machine list and line layout matched to your pipe range
  • Price and lead time in one reply
  • Test video on request before shipment
Details stay private No sales spam Maggie replies in person